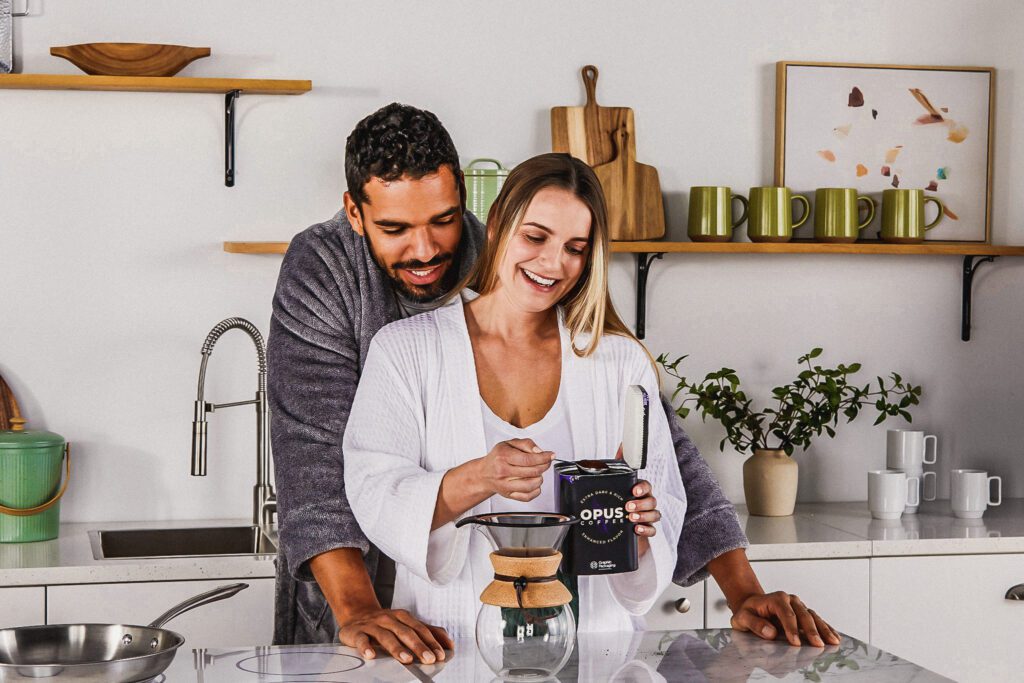
Strength Packaging
High-compression heavyweight and litho-laminated cartons engineered for wholesale club stores, heavy bulk products, and rigorous international logistics channels.

Our complete fiber-based portfolio balances high compression strength, extended barrier shelf life, automated line efficiency, and circular sustainability. Engineered to meet strict international retailer standards and high-speed filling requirements.
High-compression heavyweight and litho-laminated cartons engineered for wholesale club stores, heavy bulk products, and rigorous international logistics channels.
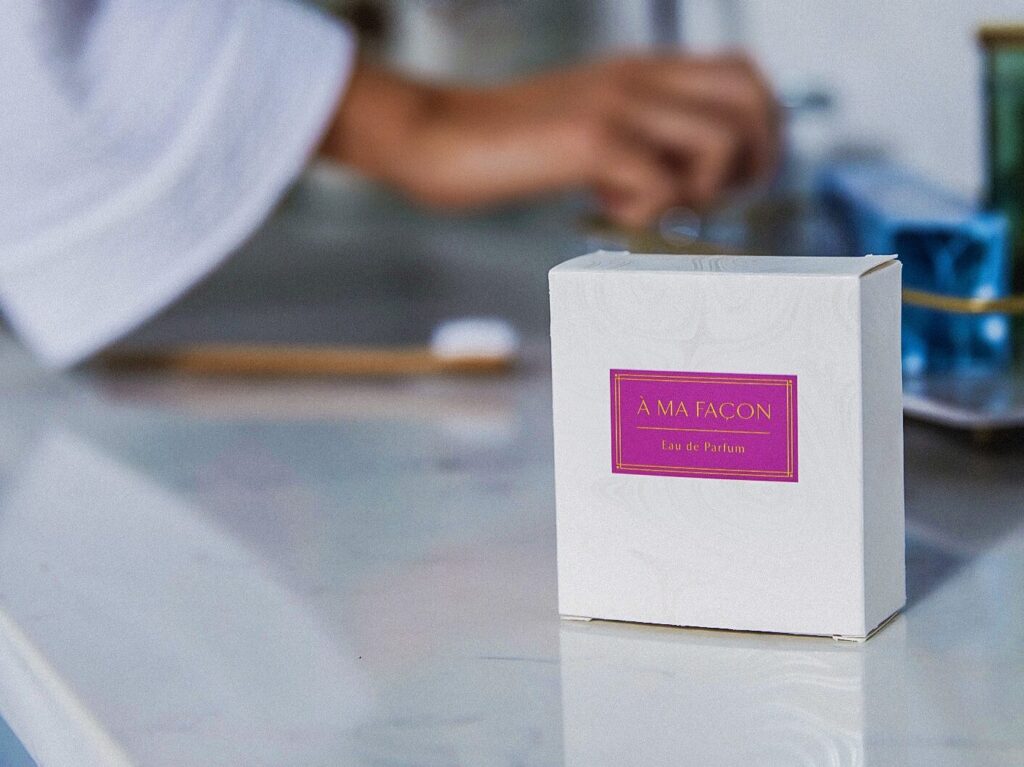
Custom structural folding cartons utilizing premium bleached, unbleached, and recycled paperboard substrates for food, dry shelf goods, personal care, and pharmaceuticals.
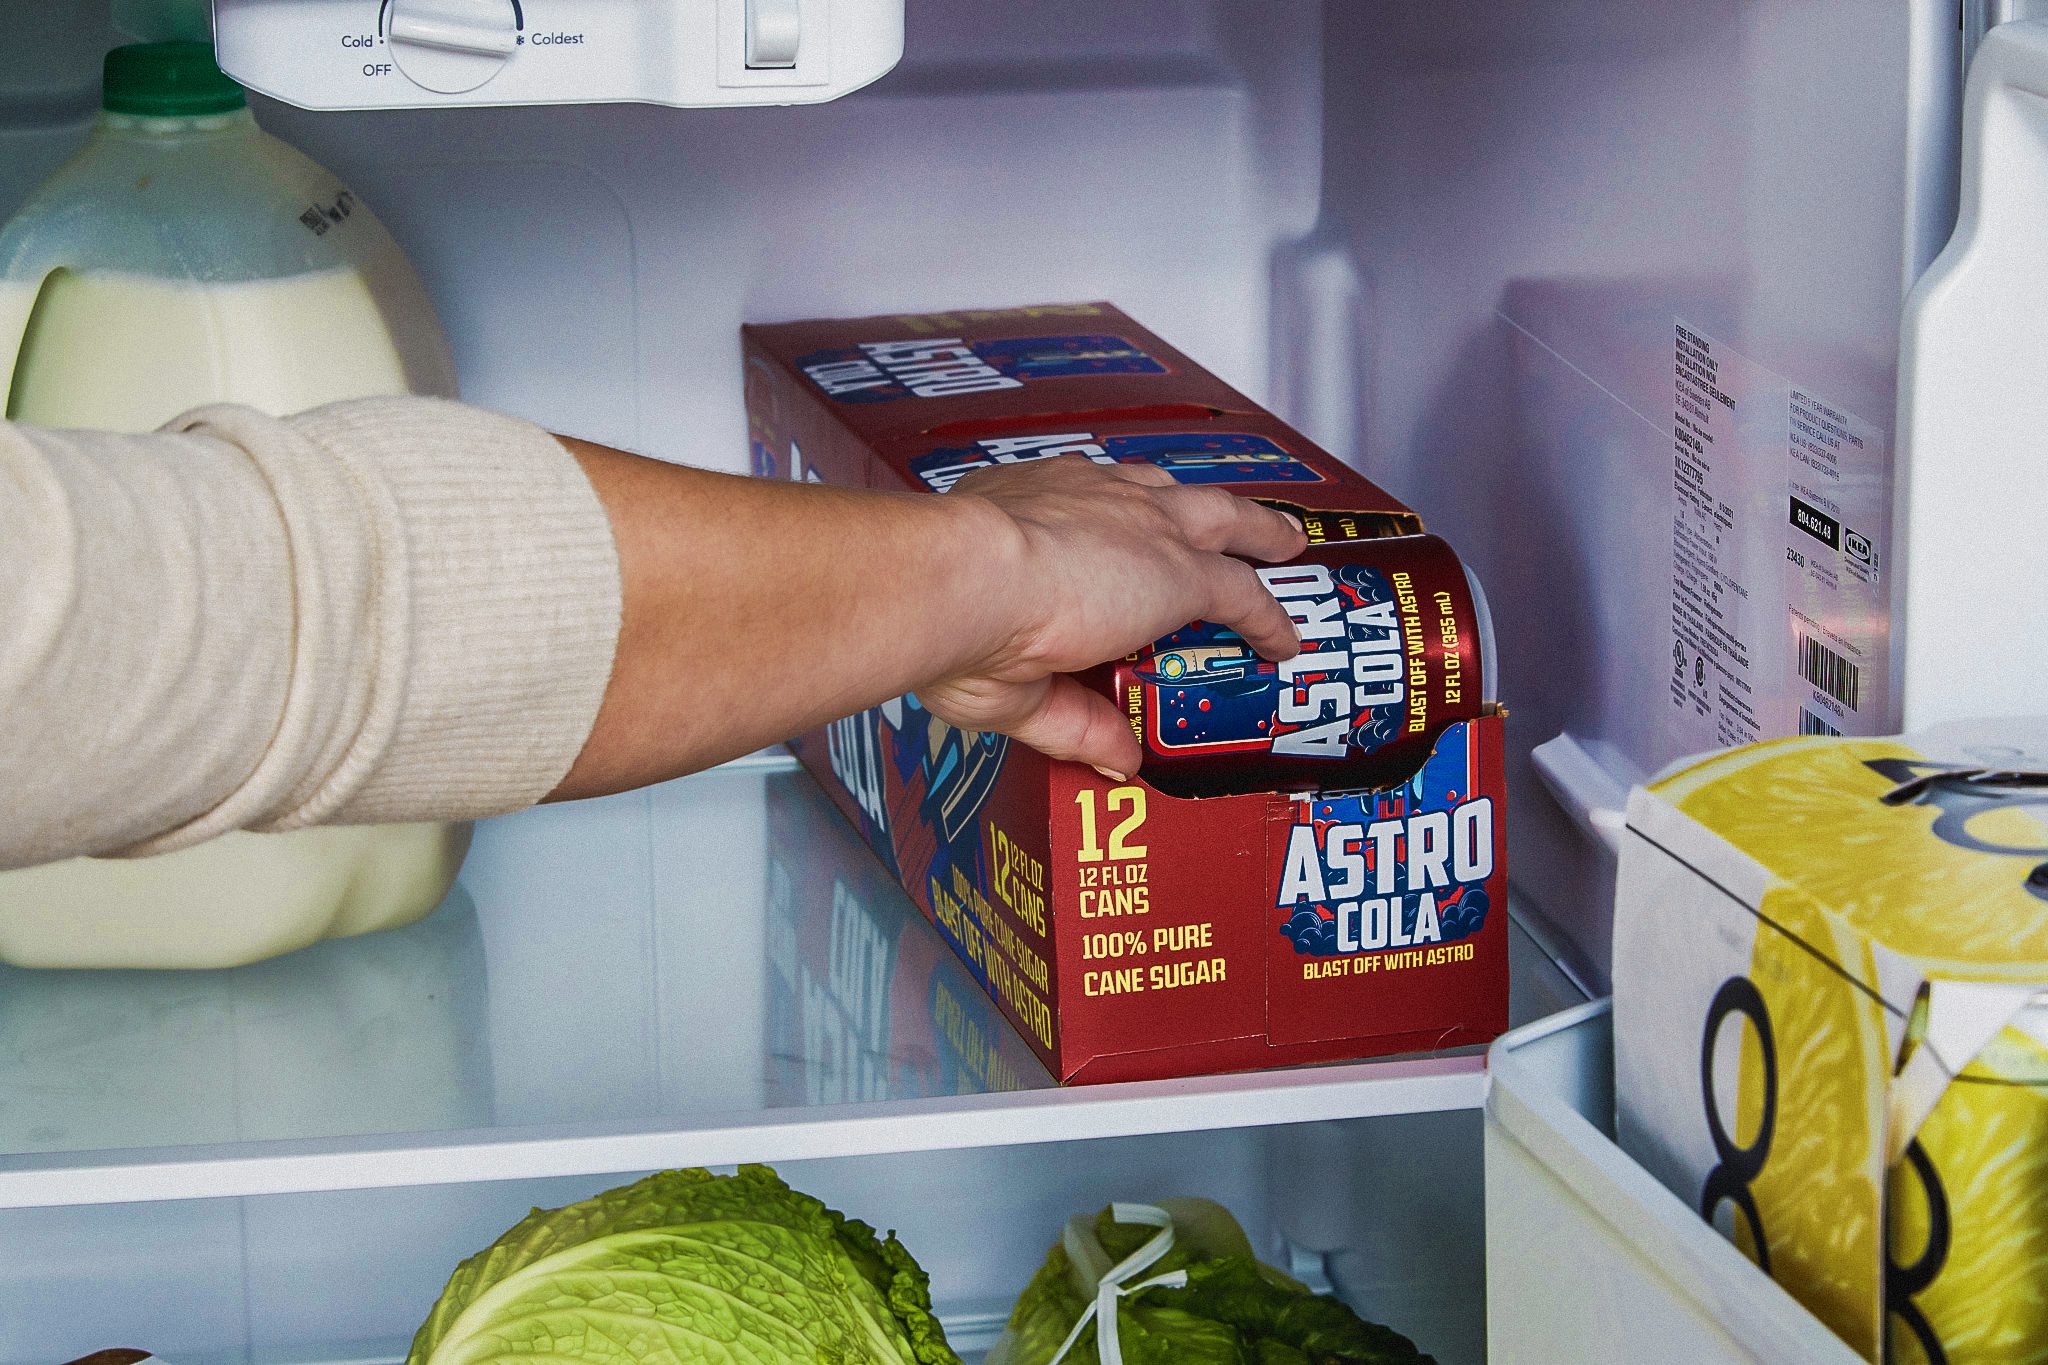
High-speed paperboard multipacks replacing plastic shrink film and rings. Formats include basket carriers, clip-style packs, wrap-around sleeves, and fully enclosed cartons for cans and bottles.
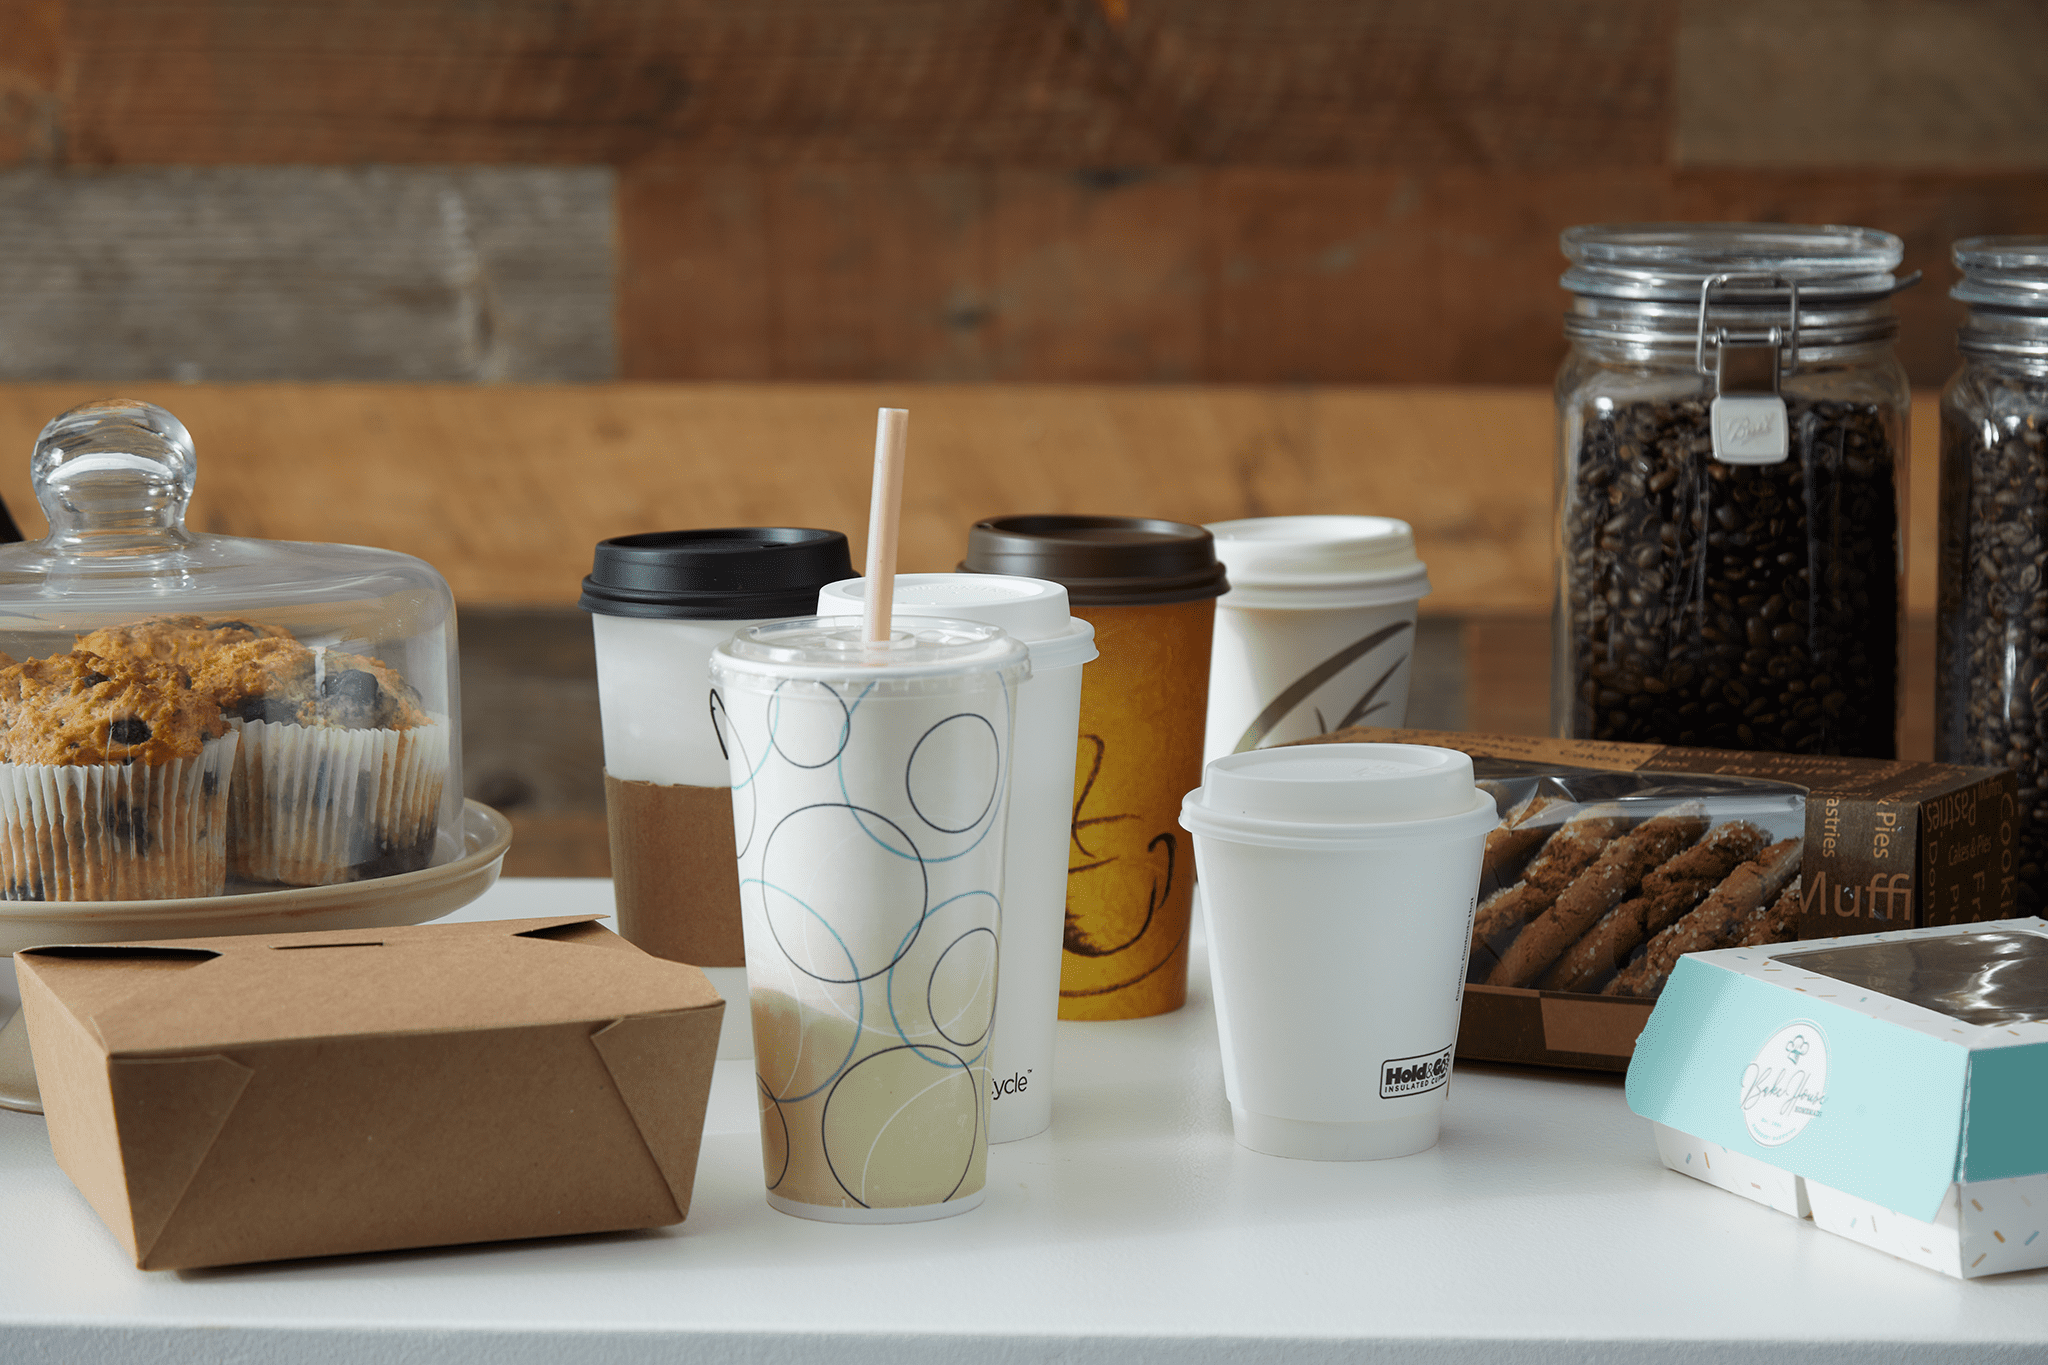
Compliance-ready food and beverage containers including hot and cold paper cups, leak-resistant lids, commercially compostable food buckets, and takeout packaging.
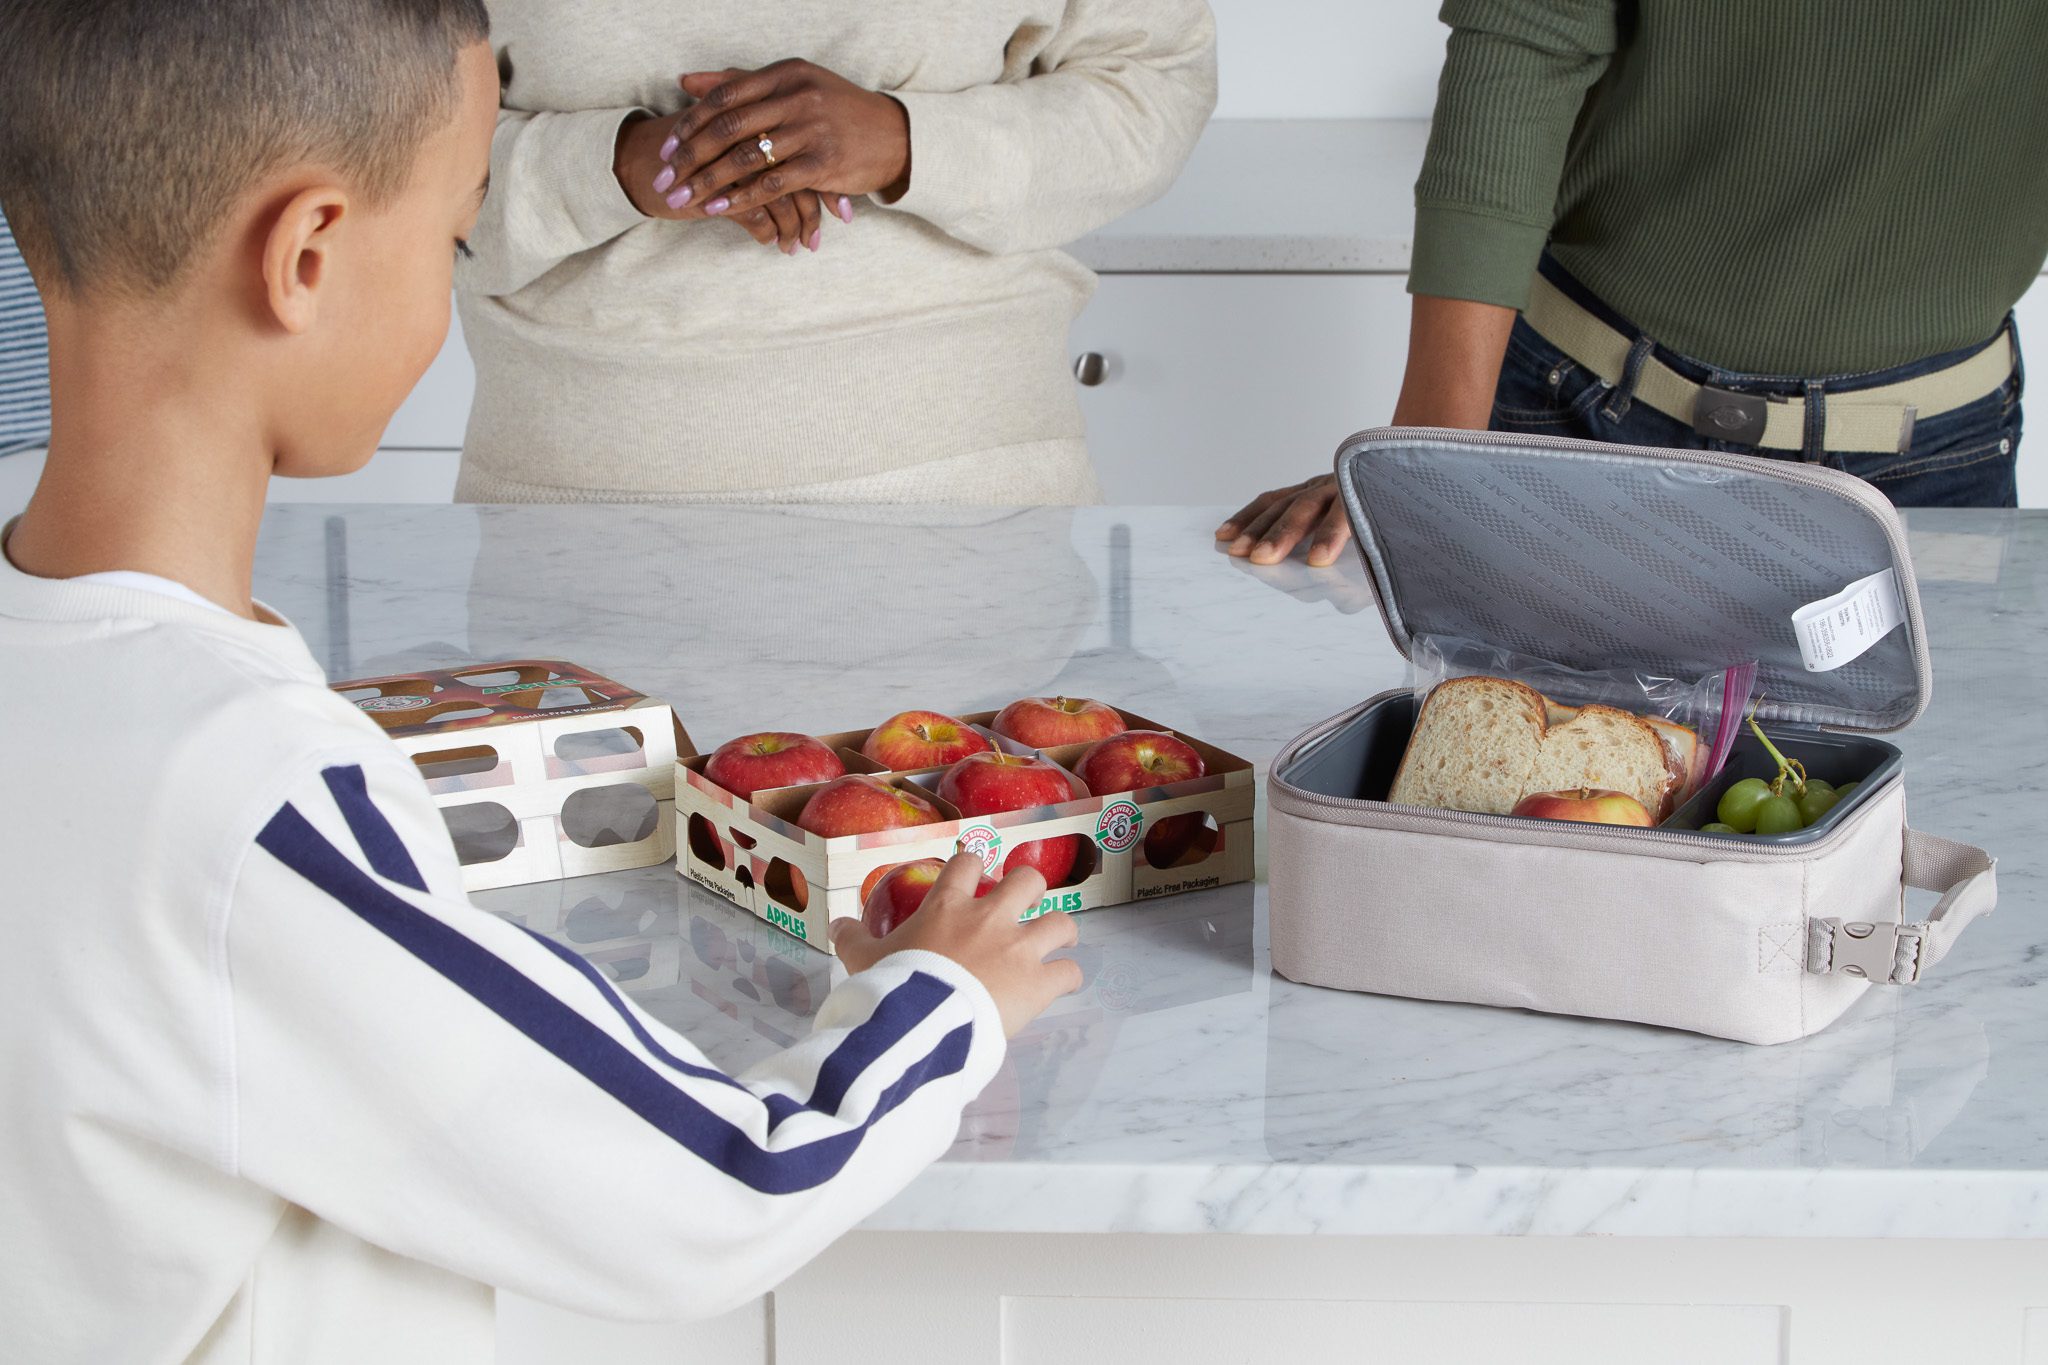
Fiber-based round tubs and hybrid barrier packs engineered with precision moisture and oxygen barriers for extended shelf-life foods like soups, ramen, and oatmeal.
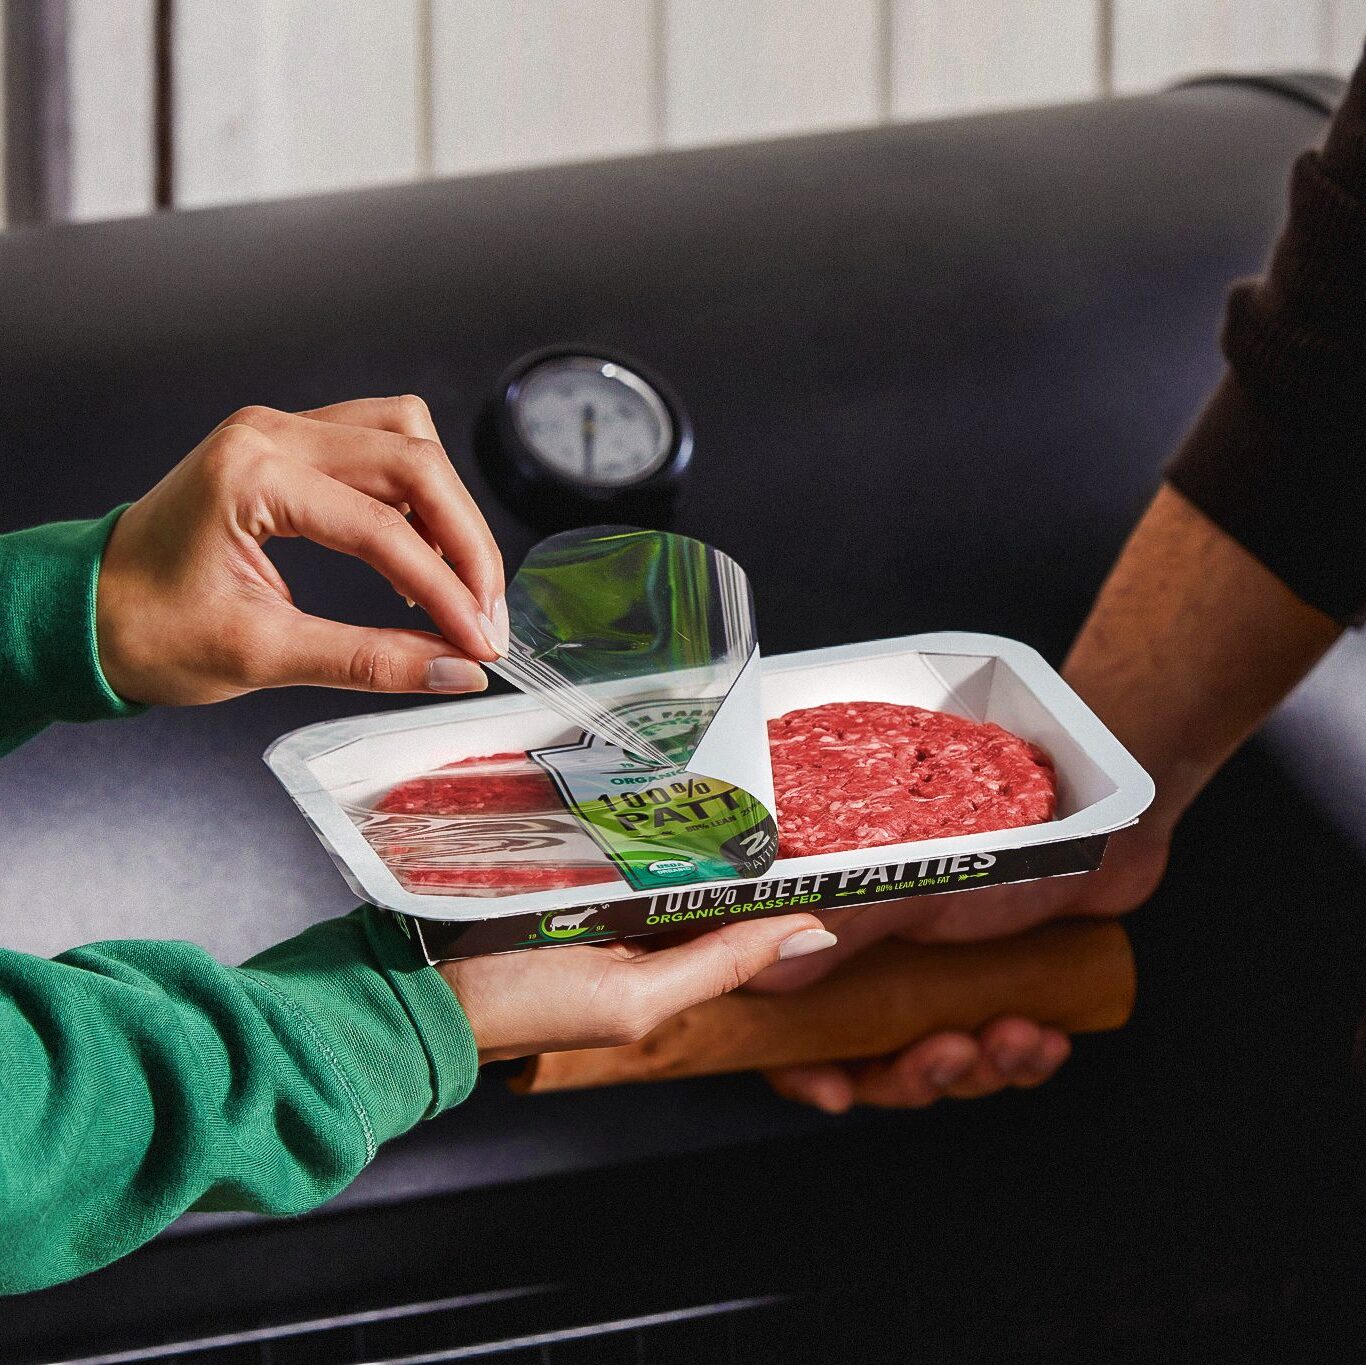
Modified Atmosphere Packaging (MAP) and top-seal barrier paperboard trays designed for fresh meats, produce, ready meals, and frozen foods, significantly reducing single-use plastic tray weight.
Advanced microwave susceptor structures, dual-ovenable pressed bowls, and baking trays providing crisping, browning, and thermal protection for convenience foods.
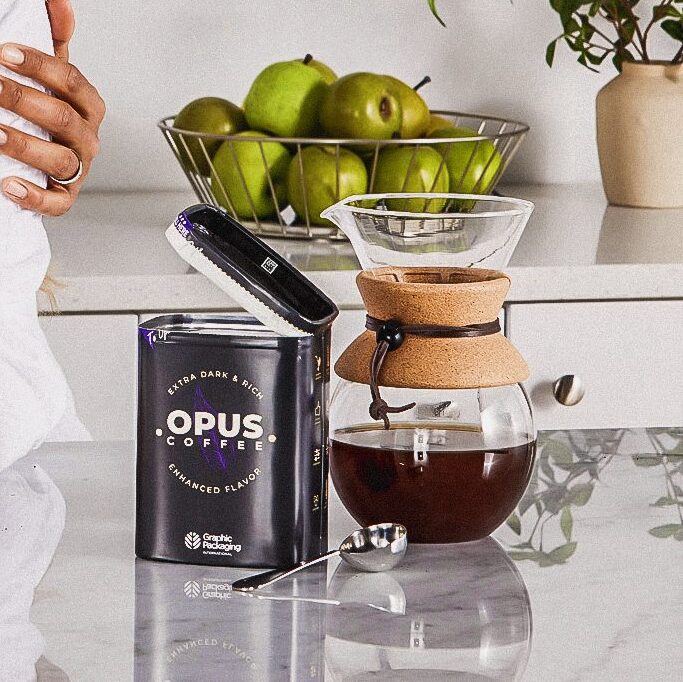
Rigid fiber canisters with customizable shapes and airtight seal barriers, serving as an eco-friendly alternative to tinplate metal cans, glass jars, and plastic tubs.
Recyclable mono-PE/PET films, high-barrier paper laminates, pouch webs, lidding films, and sterile medical packaging papers manufactured under cleanroom conditions.
Overseas procurement teams require transparent manufacturing metrics, consistent material supply, and rigorous regulatory compliance. We provide audit-ready packaging solutions backed by worldwide technical support.
ISO 9001, ISO 14001, and BRCGS global standards for food safety and packaging manufacturing consistency across all converting plants.
FSC®, PEFC™, and SFI® certified fiber sourcing with complete traceability, supporting corporate ESG compliance and plastic reduction mandates.
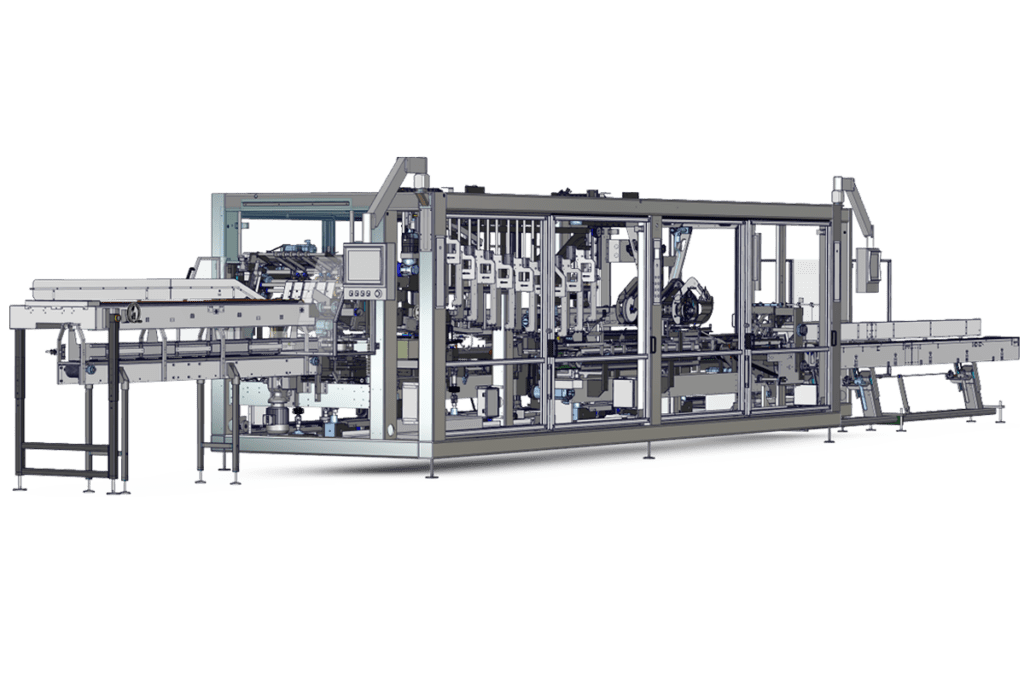
Structures specifically optimized for high-speed filling, cartoning, and multipacking lines to protect operational throughput and minimize downtime.
Multiple converting plants across North America, Europe, and Asia Pacific ensure supply chain redundancy and localized delivery for global brands.
Contact our engineering and procurement sales teams to evaluate material samples, review structural designs, or schedule a technical audit for your upcoming packaging projects.