
Explore our certified commercial-grade production lineup, optimized for high ambient stability, barrier preservation, and integrated manufacturing efficiency.
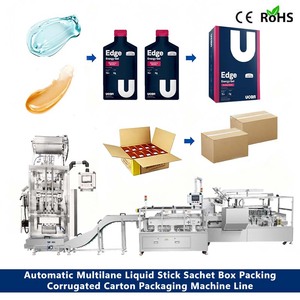
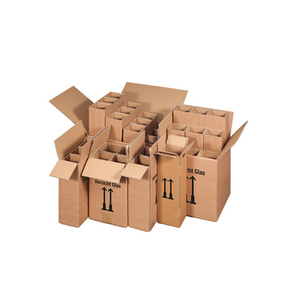
The Ghanaian industrial sector is currently undergoing a structural transformation in liquid packaging logistics. As food processing, edible oil refining, beverage manufacturing, and agrochemical synthesis expand across key industrial hubs such as Tema, Accra, Kumasi, and Takoradi, traditional rigid liquid containers—such as high-density polyethylene (HDPE) jerricans, steel drums, and glass bottles—are increasingly proving inefficient. Rigid containers present substantial operational bottlenecks, including high freight costs for un-filled inventory, susceptibility to oxygen degradation under tropical ambient humidity, high carbon footprints, and severe warehouse footprint utilization issues.
To solve these logistics and preservation challenges, enterprise supply chain directors across Ghana are transitioning to advanced Bag-in-Box (BIB) packaging systems. Combining a high-barrier flexible inner bladder with a heavy-duty outer corrugated paperboard shell, BIB packaging optimizes space, preserves liquid freshness, and drastically reduces transport-induced damage across rural and urban Ghanaian transport routes.
Bag-in-Box technology offers multi-sector versatility engineered specifically to withstand the sub-Saharan climate, characterized by ambient temperatures ranging between 26°C and 35°C and relative humidity levels often exceeding 80%. Below are the primary industrial sectors in Ghana leveraging customized BIB solutions:
Ghana’s palm oil and coconut oil processing sectors—centered around the Western and Central Regions—require sterile, light-proof packaging. Exposure to UV rays and atmospheric oxygen causes rapid rancidity in crude and refined palm oil (RPO). BIB bladders engineered with metallized PET (MET-PET) or Ethylene Vinyl Alcohol (EVOH) co-extruded films guarantee an absolute oxygen transmission rate (OTR) of < 0.5 cc/m²/day, maintaining oil clarity and chemical stability from processing plants directly to retail networks in Kumasi and Accra.
From commercial fruit juices (mango, pineapple, guava) produced in the Eastern Region to artisanal spirits like local Akpeteshie and imported commercial wines, Bag-in-Box preserves flavor integrity. The continuous pour tap mechanism (e.g., Vitop design) prevents air ingress during usage, ensuring that once opened, liquid shelf life extends from days to months—making it the ideal choice for Ghana’s expanding hospitality sector (HORECA).
Agrochemical distributors supplying Ghana’s cocoa, maize, and cashew farmers require secure containment for liquid fertilizers, pesticides, and bio-inoculants. Outer corrugated boxes engineered with high Edge Crush Test (ECT) ratings coupled with chemical-resistant linear low-density polyethylene (LLDPE) inner films eliminate transport-related ruptures along unpaved rural distribution roads.
With institutional catering, mining camps in Tarkwa and Obuasi, and educational institutions requiring sanitary bulk water supply, 10L to 20L water BIB systems provide a hygienic, tamper-evident alternative to reusable polycarbonate carboys, drastically reducing bacterial contamination risks.
The Ghanaian packaging landscape is shifting rapidly due to macroeconomic changes, regulatory enforcement, and evolving commercial practices. Supply chain directors must navigate three major trends:
The Ghana Environmental Protection Agency (EPA), alongside the Ministry of Environment, Science, Technology and Innovation (MESTI), is increasing scrutiny on single-use non-recyclable plastics. Traditional rigid plastic containers create massive plastic waste liabilities. In contrast, Bag-in-Box packaging uses up to 75% less plastic by weight than rigid containers of equivalent volume. The outer corrugated cardboard shell is 100% biodegradable and recyclable within local paper mills, positioning BIB as a preferred sustainable format for corporate ESG targets.
With fuel prices impacting long-distance road transport from the Port of Tema to inland markets and neighboring landlocked nations (Burkina Faso, Mali, Niger), payload efficiency is critical. Empty BIB packaging is shipped completely flat, allowing a single pallet to hold up to 10 times more packaging capacity compared to empty rigid drums. This dramatically reduces inbound logistics costs for Ghanaian factories.
Product counterfeiting remains a significant challenge for consumer goods brands in West Africa. High-quality Bag-in-Box packaging incorporates single-use tamper-evident spouts, custom high-resolution flexographic graphics on the outer box, and optional micro-perforated security seals, ensuring that Ghanaian consumers receive authentic, unadulterated products.
To guarantee structural integrity under tropical heat and high humidity, foreign packaging specifications cannot simply be duplicated. The outer carton and inner film must be engineered to withstand specific environmental stresses. Below is a structural engineering comparison outlining optimal specifications for the Ghanaian market:
| Specification Feature | Standard Global Specification | Ghana Market Optimized Specification | Engineering Benefit |
|---|---|---|---|
| Outer Box Fluting | Single Wall B-Flute (3mm) | Double Wall EB/BC Flute (5mm) | Prevents stacking collapse under 85%+ relative humidity in warehouses. |
| Inner Film Structure | 2-ply Standard LLDPE (50 microns) | EVOH Co-extruded 7-ply Barrier (90+ microns) | Provides a zero-light & zero-oxygen environment to stop oxidation. |
| Dispensing Tap | Basic Push Tap | Vitop Original Tamper-Evident Valve | Ensures zero-leakage, tight seal, and consumer anti-tamper security. |
| Edge Crush Test (ECT) | 32 ECT | 44 - 55 ECT (Water-Resistant Coating) | Resists puncture damage on unpaved transport corridors. |
| Filling Compatibility | Manual Gravity Fill | Semi/Fully-Automatic Aseptic Fillers | Protects biological sterility and scales processing speed. |
As a global leader in fiber-based packaging solutions and integrated packaging machinery, our organization delivers complete end-to-end operational security for Ghanaian manufacturers. We do not merely convert paperboard; we control the full value chain from raw material pulp sourcing to structural design, high-barrier pouch lamination, precision printing, and automated filling equipment integration.
Recognized globally by independent auditing bodies—including Fortune World's Most Admired Companies, Ethisphere World's Most Ethical Companies, and 3BL 100 Best Corporate Citizens—our manufacturing operations enforce rigorous quality assurance protocols under ISO 9001, ISO 22000, and BRCGS food safety standards.
We provide single-source accountability by offering both high-performance Bag-in-Box packaging materials and advanced automated filling machinery. This eliminates integration friction between material suppliers and machinery vendors, protecting your line speed and operational uptime.
Our structural design team builds tailor-made outer box dimensions, dispenser cutouts, and high-impact flexographic printing up to 8 colors. Enhance shelf appeal, reinforce brand identity, and incorporate localized compliance labeling mandated by Ghana FDA.
With extensive experience navigating customs documentation, Ghana Revenue Authority (GRA) port regulations, and shipping operations into Tema and Takoradi ports, we offer reliable lead times, strategic buffer stocking, and dedicated technical service support.
Connect with our dedicated packaging engineering specialists to request technical datasheets, sample packs, structural quotes, and customized machinery integration options for your facility.