
Precision-engineered ventilated corrugated packaging, moisture-resistant shipping cartons, and premium retail presentation boxes optimized for Kenyan agricultural export corridors.
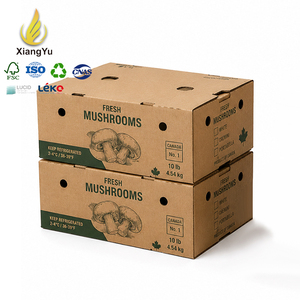
Precision air-hole layout ensures thermal equilibrium during cold chain transit. Engineered with high Edge Crush Test (ECT) Kraftliner for delicate mushrooms and greens.
Get a Quote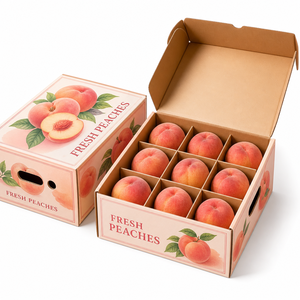
Dual-wall corrugated construction featuring soft-touch inner partitions to prevent surface bruising during farm-to-retail distribution and premium air-freight shipping.
Get a Quote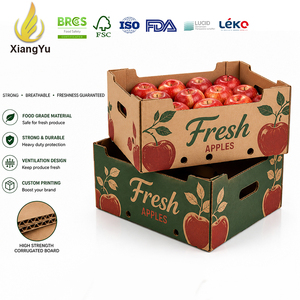
Designed for high-density stacking strength in sea freight containers. Features moisture-resistant fluting coatings to sustain vertical loads in 95% relative humidity.
Get a Quote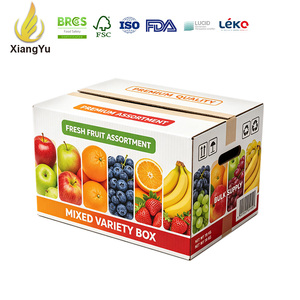
Optimized aerodynamic venting pattern prevents ethylene gas accumulation while maintaining high compression thresholds for long-haul mixed fruit export containers.
Get a Quote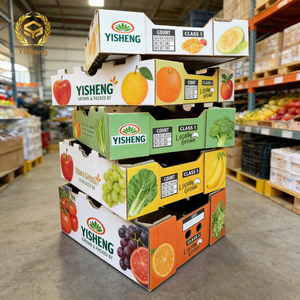
Eco-friendly fiber-based design compliant with EU packaging waste regulations. Custom flexographic water-based inks for vibrant brand visibility and zero plastic footprint.
Get a Quote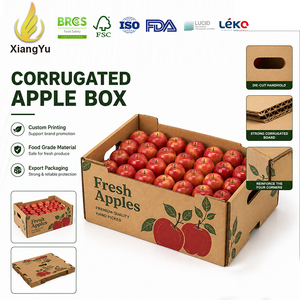
Reinforced interlocking corner pillars ensure stack integrity up to 8-high on standard pallets. Ideal for bulk transport from Kenyan orchards to processing facilities.
Get a Quote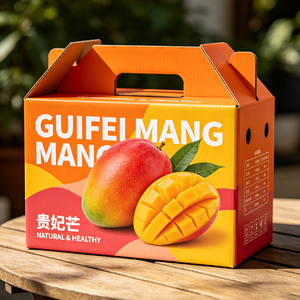
Specially coated bio-wax water barrier protection prevents moisture softening during reefer container sea transit from Mombasa to international markets.
Get a Quote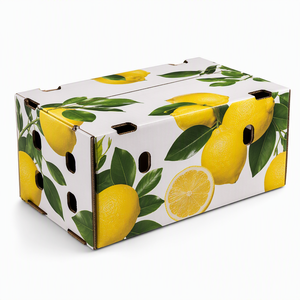
Heavy-duty B-flute and C-flute corrugated combination designed to withstand acidic peel oil release and prolonged cold storage respiration cycles.
Get a QuoteAs one of Africa's primary exporters of fresh horticultural produce—spanning fresh-cut flowers, Hass avocados, snow peas, French beans, mangoes, and passion fruit—Kenya’s agricultural ecosystem demands world-class packaging infrastructure. The Kenyan Horticultural Crops Directorate (HCD) and the Kenya Plant Health Inspectorate Service (KEPHIS) mandate stringent quality control guidelines to ensure exported goods maintain premium quality upon arrival in European, Middle Eastern, and Asian markets.
In response to international regulatory shifts, such as the European Union’s Packaging and Packaging Waste Regulation (PPWR) and single-use plastic restrictions, Kenyan growers and exporter consortiums are rapidly replacing plastic punnets, polystyrene clamshells, and non-recyclable crates with high-performance, fully recyclable fiber-based corrugated boxes.
Export shipments through Mombasa Port or Jomo Kenyatta International Airport (JKIA) undergo intense humidity shifts. Advanced water-resistant barrier coatings protect corrugated fibers from ambient condensation softening in high-humidity pre-cooling facilities.
Fruits like avocados and mangoes produce significant ethylene gas during respiration. Precision vent hole layout engineered via fluid dynamics accelerates chill rates during forced-air cooling and flushes out metabolic gases during long-haul sea freight.
Standardized box footprints compatible with 1200x1000mm air-cargo pallets and sea-container loading patterns maximize cube utilization, lowering freight-per-kilo transport overheads for local Kenyan exporters.
From Rift Valley high-altitude greenhouses to coastal fruit plantations, our produce boxes are tailored for every regional logistics challenge.
Cut roses and fresh herbs harvested around Lake Naivasha, Mount Kenya, and Eldoret require rigid long-telescopic corrugated cartons. These boxes resist heavy side-wall compression when stacked inside aircraft lower-deck pallets at Nairobi’s JKIA, preserving delicate blooms from mechanical compression.
Avocado shipments bound for Rotterdam, Fos-sur-Mer, or Jebel Ali travel 20–30 days in reefer containers. Our 4kg and 10kg open-top corrugated trays utilize heavy Kraftliners with high burst factors and bio-wax coatings to withstand continuous 4°C cold-storage condensation.
Apple Mangoes and Ngowe varieties from Eastern and Coastal Kenya require puncture-resistant fluting to prevent damage along unpaved feeder roads. Double-wall (BC-flute) corrugated boxes buffer thermal spikes and absorb kinetic impacts during transit to packhouses.
Fine beans and sugarsnap peas packaged directly for UK and EU supermarket shelves demand retail-ready corrugated packaging (RRP). Moisture-resistant printed cartons transition seamlessly from cold rooms to retail display shelves without structural sagging.
Export produce packaging is an engineered protective vessel designed to resist dynamic physical forces including static compression, transit vibration, humidity degradation, and impact shocks. Our factory utilizes virgin northern softwood Kraftliner outer facings paired with high-performance semi-chemical fluting media to ensure peak structural performance under demanding export conditions.
| Packaging Grade / Type | Flute Profile | Target Produce Category | Edge Crush Test (ECT) | Humidity Tolerance | Primary Transport Mode |
|---|---|---|---|---|---|
| Heavy-Duty Telescopic Master | BC-Flute (Double Wall) | Avocados, Citrus, Apples | 12.5 - 15.0 kN/m | Up to 95% RH | Sea Freight (Mombasa Reefers) |
| Ventilated Open-Top Tray | C-Flute (Single Wall) | Mangoes, Papayas, Melons | 8.0 - 10.5 kN/m | Up to 90% RH | Air & Maritime Containers |
| Precision Fresh Herb Box | B-Flute (Single Wall) | French Beans, Peas, Berries | 6.5 - 8.0 kN/m | Up to 85% RH | Air Freight (Nairobi JKIA) |
| Long-Stem Floriculture Carton | EB-Flute (Premium Micro) | Roses, Carnations, Lilies | 10.0 - 12.0 kN/m | Up to 80% RH | Dedicated Air-Cargo Charters |
SEO Technical Insight for Sourcing Officers: Box Compression Test (BCT) strength declines by up to 60% when ambient relative humidity increases from 50% to 90%. Our proprietary moisture-barrier coatings reduce hydro-absorption in the linerboard, preserving 85%+ of dry-state vertical column strength during long-distance cold chain shipment.
Integrating fiber-based material engineering, eco-friendly barrier technologies, and high-speed packaging equipment under one global roof.
As a world-leading fiber-based packaging producer (NYSE: GPK listed framework), our integrated operations span paperboard production, structural carton conversion, high-definition printing, and automated machinery engineering, ensuring uninterrupted supply chain security.
Our manufacturing facilities maintain international certifications including ISO 9001 (Quality Control), ISO 14001 (Environmental Management), FSC/PEFC Chain of Custody, and BRCGS Food Safety certification for direct food contact packaging compliance.
Access vanguard technologies like PaperSeal® barrier-lined paperboard trays (replacing MAP plastic trays), Boardio® rigid fiber canisters, and KeelClip™ paperboard multipack systems that eliminate plastic rings and shrink wrap.