Food Packaging Trays Manufacturer & Exporters serving the Toronto market
Engineered Fiber-Based Trays, High-Barrier MAP Containers & Sustainable Packaging Solutions for Greater Toronto & North American Supply Chains
Product Portfolio
Featured Packaging & Industrial Machinery Solutions
Explore our specialized fiber-based food trays, protective corrugated boxes, composite barrier films, and precision automated machinery designed to elevate operations across Toronto and international distribution networks.
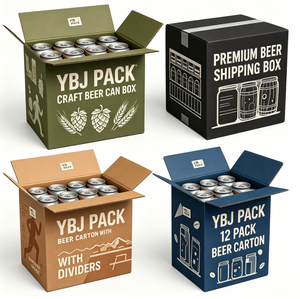
Custom 8/12 Bottle Cardboard Boxes Can Price Carton Price Beer Shipping Packaging Restaurant Beverage Box With Dividers
Why Leading Toronto Food Processors Partner With Us
PFAS-Free Barrier Technology
Advanced water-based hydrophobic dispersion coatings engineered to replace toxic fluorochemicals while providing superior oil, grease, and moisture resistance across cold and hot food applications.
High-Speed Machinery Integration
Custom-tailored paperboard tray geometries designed to run flawlessly on high-throughput automated de-nesters, conveyor lines, and top-seal vacuum skin packaging machinery.
Toronto EPR & Blue Box Optimized
Fully compliant with Ontario’s Extended Producer Responsibility (EPR) frameworks and City of Toronto kerbside recycling streams, reducing municipal disposal levies for regional brands.
Technical White Paper: The Evolution of Food Packaging Trays in the Greater Toronto Market
As the largest metropolitan economy in Canada, the Greater Toronto Area (GTA) serves as the primary processing, distribution, and retail hub for the country’s food and beverage ecosystem. Spanning key industrial nodes across Mississauga, Brampton, Vaughan, Markham, and Etobicoke, food manufacturers face dual pressures: meeting rigorous food safety standards under the Canadian Food Inspection Agency (CFIA) and complying with stringent municipal and provincial waste-reduction mandates.
As a premiere Food Packaging Trays Manufacturer & Exporters serving the Toronto market, our enterprise delivers high-performance, fiber-first packaging systems tailored specifically to the operational, climatic, and regulatory realities of Southern Ontario. The transition from legacy Expanded Polystyrene (EPS) foam and single-use Rigid Polyethylene Terephthalate (rPET) containers to renewable paperboard trays is no longer merely a branding initiative—it is a critical supply-chain requirement driven by consumer demand and statutory enforcement.
1. Regulatory Compliance Framework: Navigating Canadian & Ontario Standards
Food processing facilities operating in Ontario must align their primary and secondary packaging with multiple regulatory layers:
Safe Food for Canadians Regulations (SFCR): Enforced by the CFIA, requiring food-contact packaging materials to be chemically inert, non-toxic, and resistant to mechanical degradation during processing, cold-chain transport, and storage.
Environment and Climate Change Canada (ECCC) Single-Use Plastics Ban: Federal prohibitions targeting single-use plastic takeout containers, styrofoam trays, and non-recyclable plastic ring carriers, accelerating the shift toward pulp and paperboard alternatives.
Ontario’s Strategy for a Waste-Free Ontario & Producer Responsibility (EPR): Shifting financial responsibility for end-of-life packaging management directly onto brand owners and importers, incentivizing lightweight, highly recyclable fiber tray designs.
Our food packaging trays are manufactured in ISO 9001 and BRCGS Grade A certified facilities utilizing virgin wood fibers harvested from certified sustainable forests (FSC / PEFC) as well as premium post-consumer recycled (PCR) paperboard. Every batch undergoes rigorous migration testing to guarantee complete compliance with Health Canada’s Division 23 of the Food and Drug Regulations.
Advanced Barrier Chemistry & Structural Engineering for Food Preservation
Preserving food freshness, extending shelf life, and preventing structural collapse in moist or frozen environments are fundamental requirements for packaging exported to or manufactured within Toronto. Fresh protein packers, ready-to-eat meal kit providers, and industrial bakeries cannot afford barrier failure or tray seal degradation.
Traditional paperboard containers often struggled with gas impermeability. Our next-generation PaperSeal® class barrier-lined paperboard trays bridge this performance gap by combining a rigid, high-density paperboard chassis with a ultra-thin, removable high-barrier film layer (such as EVOH or mono-PE). This composite architecture delivers exceptional gas barrier properties:
Oxygen Transmission Rate (OTR): Less than 0.5 cm³/m²/24h, preventing lipid oxidation, color degradation, and microbial growth in fresh red meat, poultry, and deli items.
Water Vapor Transmission Rate (WVTR): Engineered down to 1.0 g/m²/24h, safeguarding dry bakery goods against humidity ingress while preventing liquid weeping in prepared food applications.
Continuous Flange Sealing: Precision die-cut top flanges ensure a 100% hermetic perimeter seal with lidding films, eliminating micro-leaks during transport across North American highway logistics networks.
Dual-Ovenable & Cold-Chain Thermal Resilience
Ontario’s seasonal temperature extremes—from -30°C winter transport conditions to hot kitchen preparation—require robust thermal stability. Our CPET-replacement pulp and paperboard trays are formulated to endure temperatures ranging from -40°C blast freezing up to +220°C (+428°F) conventional oven heating and microwave exposure without leaching volatile organic compounds (VOCs) or compromising structural stiffness.
Material Performance Comparison Matrix: Fiber-Based vs. Legacy Plastics
To assist packaging engineers, procurement managers, and operations executives in evaluating total cost of ownership (TCO) and sustainability metrics, the following data table compares our paperboard food packaging trays against conventional tray materials commonly used in the Canadian retail market.
Performance Metric
High-Barrier Paperboard Tray
Rigid CPET / APET Plastics
EPS Foam (Styrofoam)
Molded Bagasse Pulp
Virgin Plastic Content Reduction
80% – 90% Plastic Saved
0% (100% Fossil Fuel Plastic)
0% (Polystyrene Base)
100% Plastic Free
Heremetic MAP Top-Seal Integrity
Superior (Hermetic Seal)
Excellent
Poor / Not Suitable
Moderate to Poor
Temperature Tolerance Range
-40°C to +220°C (Dual Ovenable)
-40°C to +200°C
-10°C to +80°C
-18°C to +150°C
PFAS-Free Grease Resistance
Certified 100% PFAS-Free
N/A (Inherent Plastic)
N/A (Plastic)
Varies (Often contains PFAS)
Toronto Kerbside Recyclability
High (EPR Blue Box Friendly)
Moderate (Depends on color)
Banned / Non-Recyclable
Compostable Only
High-Speed Automation Compatibility
Flawless (Servo De-Nesting)
Excellent
Fragile / Static Friction
High Flange Variation
Localized Application Scenarios across Greater Toronto & Export Markets
As a global exporter with deep localized delivery capabilities throughout Ontario, we supply customized packaging tray configurations built for high-throughput commercial production lines.
Large-scale meatpacking facilities require rigid trays that resist moisture absorption from blood and purge. Our paperboard trays utilize specialized bottom-embossing patterns and optional integrated absorbent pads that immobilize fluids while presenting an appealing, premium aesthetic on supermarket shelves across Loblaws, Metro, and Sobeys stores.
Commercial caterers, hospital food service groups, and direct-to-consumer meal prep providers operating in Toronto demand multi-compartment food trays. Our precision-molded paperboard trays feature internal divider walls that prevent cross-contamination of sauces and sides, remaining firm during re-heating in high-speed microwave or convection ovens.
3. Bakery, Confectionery & Fresh Produce (Niagara & Golden Horseshoe Region)
From fragile fresh berries to dense artisanal pies and pastries, our punnet trays and corrugated folding cartons offer controlled ventilation, crush resistance during pallet stacking, and high-clarity window patching options made from home-compostable cellulose films.
4. Craft Beverage & Multipack Shipping Solutions
Supporting Ontario's thriving craft brewery and beverage sector, our heavy-duty corrugated bottle boxes and multipack cartons feature engineered drop-in dividers. Designed to withstand humid cold-storage vaults and transit vibration, these packs ensure zero bottle-to-bottle contact during urban distribution.
Corporate Authority & Supply Chain Reliability
Choosing a packaging supplier is an operational decision that directly impacts line uptime, yield rates, and brand reputation. As an industry-leading manufacturer recognized globally for corporate stewardship and manufacturing innovation, our enterprise offers unmatched structural stability:
End-to-End Vertical Integration: From primary pulp milling and paperboard manufacturing to advanced converting, barrier coating, and high-speed packaging machinery engineering, we control every link of the supply chain.
Award-Winning Industry Leadership: Consistently ranked among global benchmark organizations for ethical business practices, sustainability reporting, and technological breakthroughs (including Fortune World's Most Admired Companies, Ethisphere World's Most Ethical Companies, and 3BL 100 Best Corporate Citizens).
Global Export & Regional Warehousing: Strategic inventory hubs serving Toronto and Northeastern US trade routes guarantee just-in-time (JIT) deliveries, insulating regional plants against container shipping delays or raw material shortages.
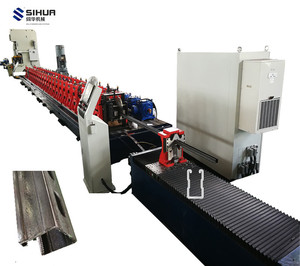
Integrated Machinery Solutions: We do not just sell packaging trays—we engineer custom servo-driven tray formers, sleeve wraparound machines, and pick-and-place robotics designed to operate synchronously with our paperboard substrates for maximum OEE (Overall Equipment Effectiveness).
Frequently Asked Questions (FAQ) – Sourcing Packaging Trays in Toronto
Below are technical answers to common questions raised by procurement managers, quality assurance executives, and packaging engineers sourcing food packaging trays for Ontario and export markets.
Are your paperboard food packaging trays certified for direct food contact by Health Canada and CFIA?
Yes. All our food contact paperboard trays, coatings, and lidding materials fully comply with Health Canada’s Food and Drugs Act and Regulations, as well as US FDA 21 CFR standards. Production facilities maintain BRCGS Grade A certifications, ensuring complete trace-ability, hygiene, and chemical migration compliance required for Canadian Food Inspection Agency (CFIA) audited facilities.
How do your barrier paperboard trays perform in cold-chain transport during Canadian winters?
Our food trays are specifically engineered with wet-strength paperboard additives and crack-resistant poly/EVOH dispersion barriers. They maintain structural rigidity and seal integrity under freezing conditions down to -40°C, preventing seal embrittlement or container wall sagging when moving through unheated logistics terminals or blast freezers across Ontario.
Can these food packaging trays replace traditional rigid plastic MAP trays on existing sealing machinery?
Yes. Our PaperSeal® barrier trays are designed with standardized outer flange dimensions compatible with major automated top-sealing machines (e.g., Mondini, ILPRA, Multivac, Sealpac). In many cases, only minor tooling updates (such as custom sealing dies or de-nesting magazines) are required to transition your line from plastic trays to fiber-based trays.
Are your grease-resistant barrier coatings completely PFAS-free?
Absolutely. In accordance with updated Canadian environmental safety regulations, our entire food tray portfolio utilizes 100% PFAS-free (per- and polyfluoroalkyl substances) aqueous acrylic and starch-based dispersion barriers that deliver high Kit-value oil, fat, and moisture resistance without hazardous fluorochemicals.
How do your products support Toronto's Extended Producer Responsibility (EPR) compliance?
Ontario’s Extended Producer Responsibility regulations penalize non-recyclable multi-layer plastics. Our paperboard trays allow consumers to easily peel off the inner barrier film lining after use, leaving clean, uncontaminated paperboard that goes directly into Toronto's kerbside Blue Box recycling system, significantly reducing your brand’s EPR fee exposure.
What lead times and minimum order quantities (MOQs) apply for custom-printed food trays exported to Toronto?
Standard stock tray dimensions feature flexible MOQs starting at pallet-level quantities. For custom structural designs or 6-color flexographic/offset branded printing, typical production lead times range from 4 to 6 weeks following proof approval. We also offer vendor-managed inventory (VMI) programs for high-volume regional processors in Southern Ontario.
Do you manufacture matching packaging machinery for automated high-volume plants?
Yes. Our machinery division designs, builds, and services custom tray formers, high-speed de-nesters, sleeve wraparound cartoning systems, and robotic case packers. By supplying both the paperboard packaging materials and the high-speed machinery systems, we ensure unified line performance and single-source accountability.
Optimize Your Food Packaging Supply Chain in Toronto Today
Partner with an industry-leading packaging tray manufacturer and exporter. Our technical sales engineers are ready to evaluate your current packaging footprint, provide complimentary sample kits, or engineer custom structural prototypes for your production line.