
Engineered to meet Sri Lanka's Central Environmental Authority (CEA) guidelines, Ceylon Tea Board export specifications, and international transit standards.
Sri Lanka’s commercial packaging sector is undergoing a structural paradigm shift driven by stringent regulatory frameworks enforced by the Central Environmental Authority (CEA), escalating international ESG compliance for exporters, and the operational demands of maritime transport through the Port of Colombo. As Sri Lanka phases out single-use expanded polystyrene (EPS) lunch boxes, plastic cutlery, and non-biodegradable polyethylene coatings under Gazette Extraordinary No. 2211/51, domestic brands and multinational exporters require advanced paperboard solutions engineered for performance, compliance, and cost-efficiency.
Key Industry Benchmark: Paperboard packaging destined for the Sri Lankan market must achieve a Cobb60 moisture absorption value of under 30 g/m² to prevent structural buckling, delamination, and microbial growth caused by average relative humidity levels exceeding 85% in Colombo, Gampaha, and coastal freight hubs.
Exporting goods from manufacturing zones such as Katunayake, Biyagama, and Koggala Free Trade Zones (FTZs) introduces extreme climatic stress. Shipments encounter intense thermal cycling and humidity transitions while moving from high-altitude plantations (e.g., Nuwara Eliya tea estates) to maritime vessel holds at the Port of Colombo. Standard virgin folding cartons without moisture barrier coatings experience up to a 45% reduction in Edge Crush Test (ECT) and Box Compression Test (BCT) values within 72 hours of exposure to tropical ambient humidity.
To counteract compressive failure during multi-tier containerized stacking, our factories utilize specialized high-density virgin Kraftliner, high-burst corrugated fluting, and aqueous dispersion barrier coatings. These engineered materials eliminate the need for traditional plastic laminates while delivering superior oil, grease, and water vapor resistance required for Ceylon Tea packaging, apparel export boxes, fresh tropical produce crates, and QSR takeaway containers.
Empowering Sri Lankan procurement managers with precise technical parameters for optimal paperboard substrate selection.
| Paperboard Material / Grade | Grammage Range (g/m²) | Moisture Cobb60 Rating | Burst Index (kPa·m²/g) | Recyclability & Regulatory Status | Primary Sri Lankan Market Application |
|---|---|---|---|---|---|
| FBB (Folding Boxboard) - Virgin Fiber | 210 - 450 GSM | < 25 g/m² (Coated) | 2.8 - 3.5 | 100% Recyclable / CEA Approved | Ceylon Tea Retail Boxes, Cosmetics, Pharma Cartons |
| CKB (Coated Kraft Back) | 230 - 500 GSM | < 20 g/m² (Heavy Barrier) | 4.2 - 5.8 | Biodegradable / Compostable Option | Beverage Multipacks, Frozen Seafood, Heavy Hardware |
| Double Kraft Heavy Corrugated (B/E Flute) | 140 - 300 GSM Fluting | < 30 g/m² | 5.5 - 7.0 | 100% Repulpable / Circular Economy | BOI Apparel Export Cartons, Logistics Moving Boxes |
| Aqueous Dispersion Coated Kraft | 250 - 400 GSM | < 15 g/m² (Water & Grease) | 3.0 - 4.5 | Home Compostable / Zero Plastic Film | QSR Takeaway Lunch Boxes, Bakery, Sushi Trays |
| Ventilated Virgin Kraftliner (C Flute) | 170 - 250 GSM | < 28 g/m² | 4.8 - 6.2 | 100% Recyclable Paperboard | Fresh Tropical Fruit, Mushroom & Vegetable Export |
Multi-layered fluting structures engineered to maintain stackability under heavy tropical humidity. Prevents container collapse during long-distance ocean freight from Colombo Port to Europe, North America, and the Middle East.
Eliminate traditional polyethylene (PE) and aluminum foil laminates. Our water-based dispersion barriers deliver grease resistance (Kit Level 12) and vapor protection while remaining 100% repulpable in standard paper mills.
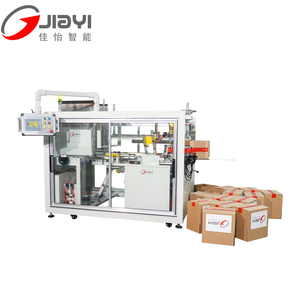
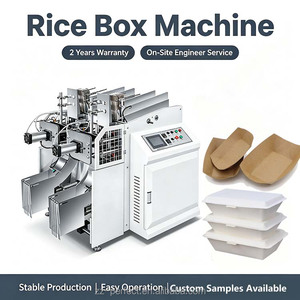
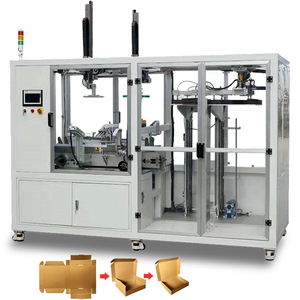
Carton blanks and folded boxes produced with sub-millimeter precision tolerances, ensuring seamless feeding into automatic case erectors, tray formers, and high-speed filling lines without jam risks.
Tailored paperboard engineering for Sri Lanka’s primary export revenue drivers and rapidly modernizing domestic urban markets.
Challenge: Retaining volatile aroma compounds, preventing moisture ingress, and meeting luxury aesthetic demands in international markets.
Solution: High-barrier FBB folding cartons with metallic cold-foil embellishments, embossed finishes, and odor-neutral barrier liners certified for direct tea contact (ISO 22000 compliant).
Challenge: Protecting high-value textile garments against compression creases, humidity degradation, and pilferage during multi-modal export shipping.
Solution: Heavy-duty, high-ECT corrugated master cartons and flat kraft gift boxes engineered for automated case erect systems in Katunayake and Biyagama Free Trade Zones.
Challenge: Preserving humidity balance for exported papayas, mangoes, pineapples, and mushrooms shipped via Bandaranaike International Airport (CMB).
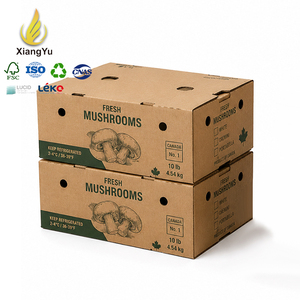
Solution: Precision die-cut, ventilated corrugated paperboard boxes featuring moisture-resistant Kraftliner and reinforced corner posts for optimal stack stability in cold storage.
Challenge: Replacing banned expanded polystyrene (EPS) takeaway containers with leak-proof, food-grade biodegradable paper structures.
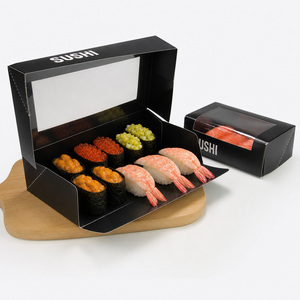
Solution: Double-station formed kraft food trays, clamshell boxes, sushi boxes with biodegradable clear windows, and aqueous dispersion meal kits designed for urban delivery services.
Challenge: Preventing essential oil migration through paper fibers and shielding delicate spices from ambient moisture contamination in Matale and Kandy hubs.
Solution: High-barrier composite paper canister board and BOPET/Paper rigid boxes featuring oil-resistant inner liners and hermetic induction sealing capabilities.
Challenge: Packing heavy, sharp metal components without tearing or puncturing the outer paperboard casing during internal logistics.
Solution: Heavyweight solid unbleached kraft cartons paired with automated case erector systems for seamless assembly line integration in Sri Lankan assembly plants.
Maximizing throughput, minimizing labor overhead, and eliminating material wastage with matched packaging machinery.
Procurement strategy in modern manufacturing requires treating packaging material and packaging equipment as a unified system. Operating high-speed production lines in Sri Lanka without matched carton blank geometry and machine tolerances leads to excessive line downtime, misfeeds, and high scrap rates.
Why leading Sri Lankan brands and international buyers partner with our certified manufacturing facilities.
Every production batch undergoes comprehensive testing for Edge Crush Test (ECT), Ring Crush Test (RCT), Cobb Moisture Absorption, Bursting Strength (Mullen Test), and Odor Neutrality to ensure zero defect rates upon delivery to Sri Lankan ports.
100% of our paperboard options originate from responsibly managed forests. Full Chain of Custody (CoC) certification guarantees compliance with EU Deforestation Regulation (EUDR) for Sri Lankan exporters shipping to European markets.
Manufactured in food-grade environments adhering to BRCGS Global Standard for Packaging Materials, ISO 9001 Quality Management, and ISO 14001 Environmental Management Systems.
Clear answers regarding logistics, customs tariffs, minimum order quantities, and moisture protection.
Connect directly with our senior packaging engineers to review technical drawings, request free physical samples, or receive a customized quotation for your factory’s volume requirements.