
Explore our precision-engineered thermoforming rigid sheets, protective fresh produce cartons, retail paperboard packaging, and high-speed vertical cartoning machinery supplied across Melbourne and global markets.
In the rapidly evolving industrial ecosystem of Greater Melbourne and Victoria, food processing, beverage production, pharmaceutical manufacturing, and agricultural export sectors face unprecedented cost pressures. As manufacturers shift toward automated end-of-line packaging, selecting a qualified global manufacturer and exporter of cartoners and carton formers serving Melbourne becomes a central strategic decision. Secondary packaging is no longer merely a transport container; it is an integrated engineering framework that directly impacts overall equipment effectiveness (OEE), retail shelf presence, cold-chain integrity, and environmental compliance.
Modern automated cartoning machinery encompasses a diverse array of structural formers, horizontal end-load cartoners, vertical top-load cartoners, tray formers, and multipack wrapping systems. Whether handling delicate fresh fruit punnets in the Yarra Valley, high-speed dairy cartons in Campbellfield, or blister packs in Parkville’s biomedical precinct, our machinery systems are engineered to synchronize mechanical speed with structural paperboard physics. By unifying custom box design, high-barrier rigid substrates, and servo-driven mechanical tuck-in/hot-melt gluing systems under a single OEM engineering architecture, we mitigate line stoppages, eliminate carton jamming, and maximize throughput efficiency.
Information Gain Key Metric: Single-source alignment between carton structural tooling and machinery mechanical kinematics reduces line commissioning times by up to 35% and eliminates operational friction between packaging converters and equipment vendors.
Industrial cartoners operate at speeds ranging from 60 to upwards of 450 cartons per minute (CPM). Achieving this output requires precise mechanical synchronization:
Melbourne’s manufacturing footprint spans distinct regional nodes, each presenting unique mechanical and environmental requirements for cartoners, tray formers, and protective corrugated packaging.
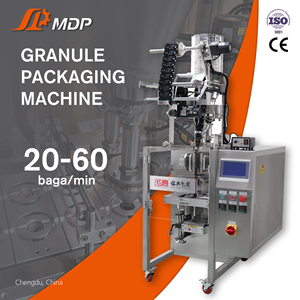
Victoria’s major food manufacturing facilities require heavy-duty corrugated tray formers and continuous-motion end-load cartoners designed for high-humidity washdown environments. Applications include fully automated loading of flexible pouches, frozen meal trays, and bakery items into retail-ready shelf cartons. Our vertical granule packing machines and tape-free corrugated boxes streamline fast-moving consumer goods directly onto pallets bound for national supermarket distribution centers in Truganina and Altona.
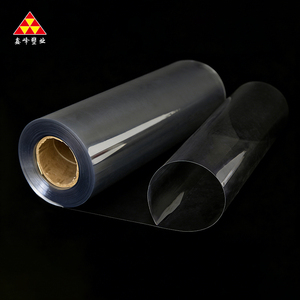
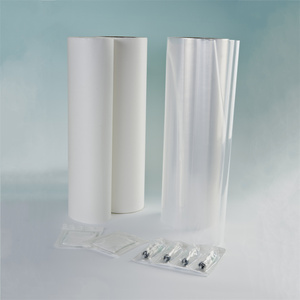
Pharmaceutical cartoning demands uncompromising precision, serialization integration, and child-resistant locking structures. Serving Melbourne's healthcare sector, our intermittent-motion horizontal cartoners incorporate vision system cameras, barcode validation, and automatic leaflet insertion. Coupled with medical-grade PP/PE blister thermoforming film, our cartoners ensure compliance with TGA (Therapeutic Goods Administration) standards while offering tamper-evident security.
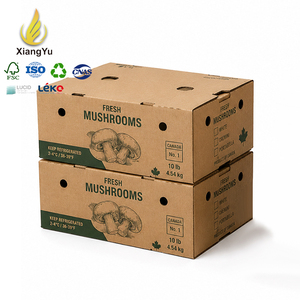
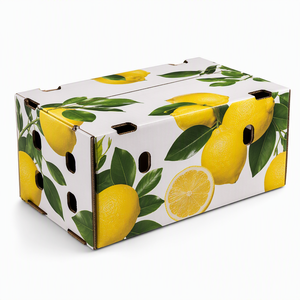
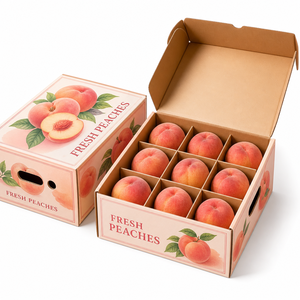
Victoria is Australia’s leading exporter of fresh horticultural produce, sending lemons, peaches, citrus, and mushrooms across Asia-Pacific. Agricultural packhouses require field-deployable corrugated tray formers capable of handling ventilated fresh vegetable and fruit boxes. Our custom vented citrus shipping cartons and fruit gift boxes are engineered to withstand stacking pressures in refrigerated sea containers routed through the Port of Melbourne.
From boutique wineries to high-volume beverage canning lines, automated wrap-style and basket carrier multipack machines replace plastic shrink wrap with recyclable paperboard clips and fully enclosed multipack cartons. Our equipment handles glass bottles and aluminum cans with zero scuffing, reinforcing premium brand aesthetics while lowering packaging mass.
Australia’s packaging sector is undergoing a profound structural shift driven by national regulatory mandates, labor cost dynamics, and sustainable supply chain imperatives. Manufacturers and importers in Victoria must align their production lines with several key macro trends:
The Australian Packaging Covenant Organisation (APCO) has mandated strict national packaging targets, requiring 100% of packaging to be reusable, recyclable, or compostable, while phasing out problematic single-use plastics. For Melbourne procurement officers, replacing plastic shrink bands and non-recyclable composite trays with fiber-based paperboard solutions is an urgent priority. Our high-barrier PET thermoforming rigid sheets, 100% recyclable kraft corrugated moving boxes, and paperboard basket carriers directly support corporate ESG metrics and APCO audit compliance.
Elevated wage rates and persistent labor shortages in Melbourne’s industrial west and south-east have accelerated the adoption of automated carton formers, robotic pick-and-place systems, and automatic vertical pouch filling machinery. Transitioning from manual hand-erecting of corrugated boxes to an automated carton former capable of erecting 40 cases per minute yields a rapid return on investment (ROI), often realized within 9 to 14 months of operational deployment.
Exports leaving Swanson Dock and Victoria Dock face rigorous multi-climate transit routes. Moisture absorption in standard corrugated paperboard can lead to box compression failure in high-humidity shipping containers. Our ventilated fruit packaging cartons utilize wet-strength kraft liners, water-resistant starch adhesives, and specialized structural stacking shoulders to maintain structural integrity across long ocean freight voyages.
When sourcing high-capital packaging equipment and enterprise-grade carton supplies for Australian facility installations, establishing supplier trust, technical authority, and long-term service stability is essential. As a publicly traded leader (NYSE: GPK) in fiber-based packaging systems, our operational performance is audited and recognized by global institutions:
Our integrated manufacturing lifecycle covers paperboard pulping, barrier coating formulation, structural CAD design, precision converting, high-speed rotary printing, and end-of-line machine building. By eliminating third-party converter friction, we ensure that every corrugated fruit box, blister film, and vertical granule packing machine operates under strict quality management systems (ISO 9001, BRCGS Food Safety Standard, and HACCP compliance).
CleanClose™ with ChildBlock™ paperboard packaging is certified under 16 CFR § 1700.20 standards. Designed for laundry pods, pharmaceuticals, and household chemicals, offering adult accessibility combined with child safety.
KeelClip™ paperboard clip multipack solutions replace single-use plastic ring carriers on beverage lines, while PaperSeal™ trays offer barrier-lined paperboard options to replace MAP plastic trays in fresh meat and protein packaging.
Key operational, technical, and logistical questions addressed for engineering managers, procurement specialists, and plant directors across Victoria:
Consult with our senior packaging machinery specialists to analyze your carton profiles, speed requirements, and plant floor layout. Request a tailored quotation or machine demonstration today.
Inquire Now