Panama Beverage Packaging Outlook: Market Dynamics, Climate Resilience, and Regulatory Drivers
Panama occupies a uniquely strategic position in the Latin American beverage sector. As the logistics crossroads of the Americas anchored by the Panama Canal, Tocumen International Cargo Hub, and the Colón Free Zone (Zona Libre de Colón), Panamanian beverage manufacturers, contract packers (co-packers), and distributors require high-performance secondary packaging solutions capable of surviving rigorous multi-modal transport while meeting stringent retail merchandising standards in metropolitan hubs like Panama City, San Miguelito, and David.
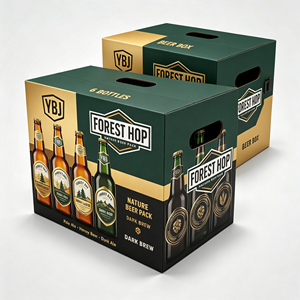
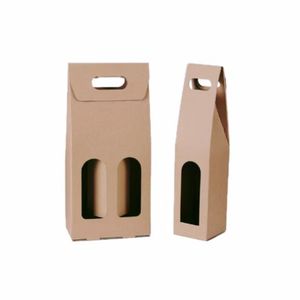
The demand for basket carrier multipacks—specifically 4-pack, 6-pack, and 8-pack die-cut handles engineered for glass bottles and aluminum cans—is surging exponentially. Panamanian consumer preferences are shifting rapidly toward premium craft beers, imported carbonated soft drinks (CSDs), RTD (Ready-To-Drink) cocktails, functional beverages, and gourmet cold-brew coffees. However, procuring paperboard basket carriers for Panama presents distinct operational challenges that generic packaging converters fail to address.
Information Gain Insight for Panama Sourcing Managers: Panama's tropical maritime climate maintains an average relative humidity (RH) exceeding 85% with ambient temperatures hovering between 28°C and 34°C year-round. Standard clay-coated recycled paperboard (CRB) quickly absorbs atmospheric moisture, causing structural softening, handle tear-outs, and bottom-lock collapses during transport between air-conditioned distribution centers and humid ambient retail environments. OEM basket carrier manufacturers must supply Coated Unbleached Kraft (CUK) with high wet-strength resin sizing to guarantee zero structural failure.
Compliance with Panama Law 187 on Single-Use Plastics
Under Panama’s national regulatory framework (Ley 187 de 2020), which progressively regulates and prohibits single-use plastic items, commercial beverage brand owners are facing escalating regulatory pressure to eliminate plastic ring carriers (Hi-Cone style) and non-recyclable shrink wrap films. Global and domestic beverage brands operating in Panama City supermarket chains such as Super 99, Riba Smith, Supermercados Rey, and Xtra are aggressively replacing plastic with 100% paperboard basket carriers and clip-style cardboard multipacks to avoid environmental tax fines and enhance ESG consumer alignment.
Structural Engineering of Heavy-Duty Basket Carrier Multipacks
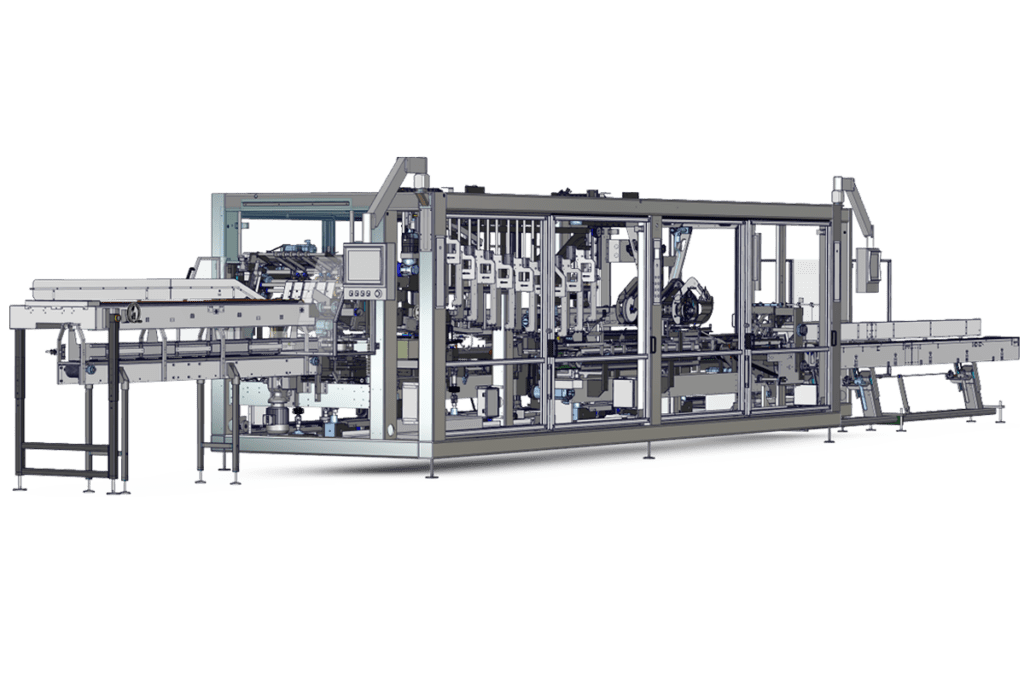
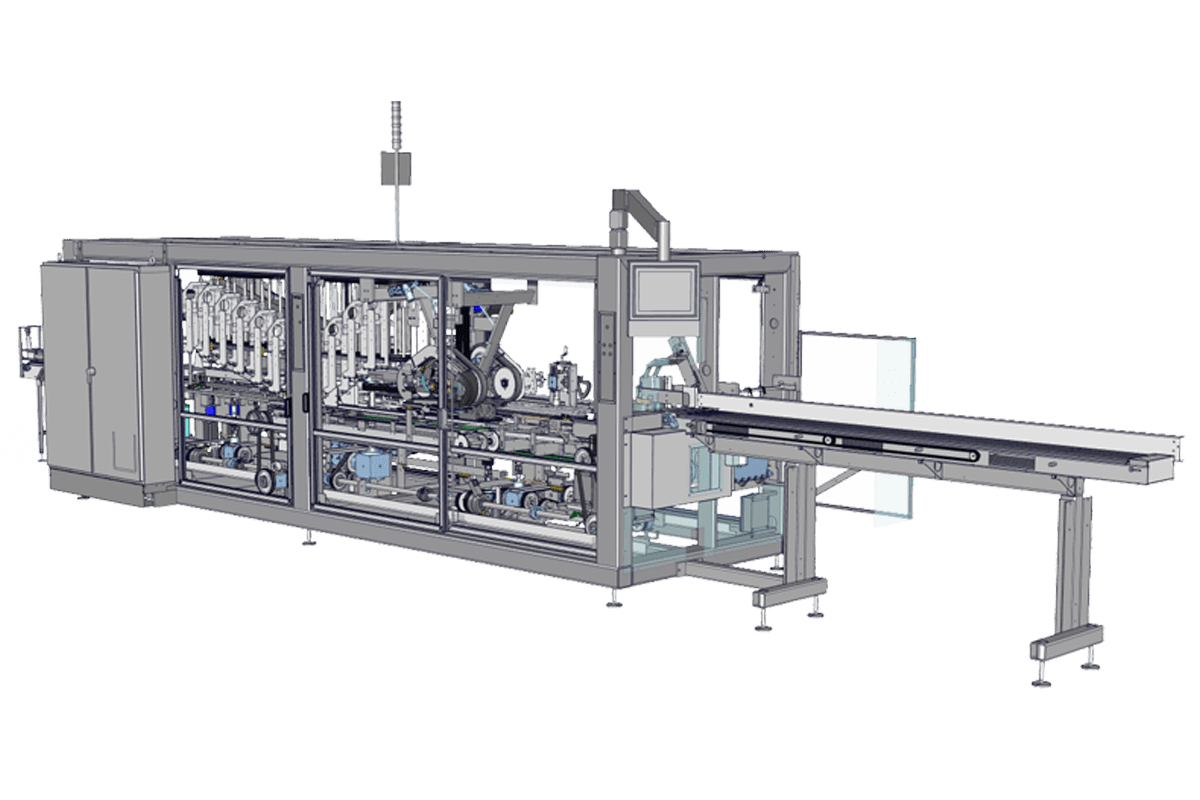
Our factory engineers basket carrier multipacks designed specifically for automated high-speed cartoning machines (such as Autoflex™ and QuikFlex™ systems) as well as manual/semi-automated filling operations utilized by microbreweries. Below is a comprehensive engineering breakdown of the material science and structural features integrated into our carrier designs:
Key Structural Features
Wet-Strength CUK Paperboard: Manufactured with virgin pine wood fibers and wet-strength chemical additives, providing superior tear resistance and burst protection under condensation.
Reinforced Ergonomic Handle Geometry: Multi-ply folded top handles distribute force evenly across the carrier structure, preventing finger-pinch and torn handles under 6-bottle payloads (up to 3.5 kg).
Auto-Locking Crash Bottom: Pre-glued precision bottoms pop open instantly on automated packing lines, ensuring structural integrity under high dynamic drop forces.
Integral Center Partitions: Full-depth or partial-depth paperboard cell dividers isolate individual glass bottles, eliminating bottle-to-bottle contact, glass clinking, and transit breakage.
Data Visualization: Material Grade Comparison for Panamanian Import
Performance Specification
Standard CRB (Recycled Board)
High-Yield CUK (Virgin Fiber Kraft)
Heavy-Duty Micro-Flute Corrugated
Caliper / Thickness Range
18 pt - 24 pt (0.45mm - 0.60mm)
16 pt - 28 pt (0.40mm - 0.70mm)
E-Flute / F-Flute (1.1mm - 1.5mm)
High-Humidity Retention (85% RH)
45% (High Risk of Softening)
94% (Exceptional Moisture Barrier)
88% (High Rigidity)
Tear Resistance (Mullen Burst)
175 - 225 PSI
350 - 480 PSI
420 - 550 PSI
Automated Machine Compatibility
Up to 400 packs/min
Up to 1,200 packs/min
Up to 250 packs/min
Recyclability & Eco-Tax Exemption
100% Recyclable
100% Recyclable & Compostable
100% Recyclable
Regional Applications
Tailored Packaging Solutions Across Panama
From craft breweries in Chiriquí to major commercial bottling plants in Panama City, our basket carriers deliver targeted performance for local distribution networks.
Panama City Supermarket & Retail Cold Chain
Engineered with hydrophobic barrier coatings to endure sudden temperature drops when moving from unconditioned delivery trucks into refrigerated walk-in display cases at Riba Smith and Super 99.
Colón Free Zone (Zona Libre) Re-Export Hub
High-density palletizable corrugated and fiberboard master cartons designed for re-export logistics from Colón to Central America and the Caribbean, featuring anti-counterfeiting UV inks.
Boquete & Chiriquí Craft Brewery Hubs
Custom short-run, 4-color offset printed 4-packs and 6-packs for independent craft brewers producing artisan ales, hard seltzers, and cold-brew beverages in highland tourist regions.
Why Direct-from-Factory Sourcing Beats Local Brokerage
Procuring basket carrier multipacks directly from our certified manufacturing facility provides Panamanian beverage companies with complete supply chain transparency, direct engineering support, and significant cost advantages. Backed by corporate achievements including Fortune World's Most Admired Companies 2026, Ethisphere World's Most Ethical Companies 2026, and JUST Capital recognition, our production infrastructure satisfies the highest audited compliance standards.
Integrated Machinery & Packaging Systems
Unlike brokers who sell paperboard cartons isolated from production line realities, our factory designs paperboard structures and high-speed packaging equipment in tandem. Whether your line operates at 100 packs per minute or 1,200 cans per minute, our basket carriers feature exact scoring, precise die-cut tolerances, and COF (Coefficient of Friction) coatings optimized for high-speed automated feeders.
We provide full OEM/ODM customization: from structural CAD dieline creation to high-definition 8-color flexographic and offset printing, metallic foil stamping, tactile embossing, and water-based barrier coatings.
Procurement Pathway
5-Step Direct Factory OEM Workflow
A streamlined, risk-mitigated process for Panama beverage brands, importers, and co-packers.
01
Dieline & Brief Audit
Submit your bottle/can dimensions, pack count (4/6/8 pack), line speed, and retail targets.
02
CAD Prototyping
We engineer custom 3D dielines and supply physical unprinted samples for drop & fit testing.
Direct containerized delivery to Port of Balboa (Pacific) or Port of Manzanillo / Cristobal (Atlantic).
Sourcing FAQs
Frequently Asked Sourcing Questions
What is the minimum order quantity (MOQ) for custom-printed basket carrier multipacks shipped to Panama?
Our standard MOQ for custom offset or flexographic 4-color printed basket carrier multipacks is 20,000 units per artwork variation. For high-volume commercial runs (100,000+ units), we offer optimized container-load pricing (20ft / 40ft HQ FCL) directly to Puerto Balboa or Puerto Manzanillo.
How do your basket carriers hold up under Panama's extreme tropical humidity?
We specify Coated Unbleached Kraft (CUK) virgin paperboard formulation integrated with wet-strength resins and hydrophobic barrier coatings. This prevents moisture penetration and strength loss even when carriers are exposed to 85%+ relative humidity during transit or cold-chain condensation.
Can your factory supply both the paperboard basket carriers and the packaging machinery?
Yes. We provide integrated packaging systems including high-speed basket multipack machinery (such as Autoflex™ series), sleeve wrapping equipment, and cartoning machinery designed to run our exact board calipers with zero downtime.
Are these basket carrier multipacks compliant with Panama Law 187 eco-regulations?
Absolutely. Our basket carriers are made from 100% fiber-based substrates sourced from certified sustainable forests (FSC / PEFC). They contain zero single-use plastic, are 100% curbside recyclable, and fully comply with Panama Law 187 plastic reduction rules.
What shipping ports and logistics arrangements are available for Panamanian importers?
We ship via FOB, CIF, or DDP terms. Regular ocean freight shipments land at Puerto Balboa (Pacific side, convenient for Panama City bottling plants) or Manzanillo International Terminal / Colón Container Terminal (Atlantic side, ideal for Colón Free Zone re-export operations).
Accelerate Your Beverage Packaging Strategy in Panama
Request custom CAD samples, wet-strength technical datasheets, and direct factory pricing tailored to your bottle or can packaging lines.