Engineered to support Singaporean food manufacturers, central kitchens, HORECA distributors, and bulk chemical packagers demanding zero-leakage security and extended shelf life.
In high-density industrial hubs like Jurong, Tuas, and Senoko, land premiums and logistics efficiency dictate packaging strategy. Bag-in-Box technology delivers measurable operational superiority.
Singapore occupies a unique position in global trade as Southeast Asia's primary food manufacturing, re-export, and chemical distribution hub. However, enterprise food processors in industrial estates such as JTC Food Hub @ Senoko, JTC Bedok Food City, and the Tuas Industrial Estate operate under intense cost pressures driven by high industrial real estate rents, stringent Singapore Food Agency (SFA) hygiene standards, and ambitious zero-waste initiatives overseen by the National Environment Agency (NEA).
Traditional liquid containers—such as 20-liter rigid HDPE jerrycans, steel drums, and glass carboys—impose significant financial drag on Singaporean enterprises. Empty rigid containers incur exorbitant storage fees per square meter of warehousing space and add dead weight during sea and land transport from neighboring markets such as Malaysia and Indonesia. As a premier Bag-in-Box (BIB) manufacturer and global exporter, we provide engineered liquid packaging systems specifically tailored to overcome Singapore’s climate, regulatory, and supply chain challenges.
Information Gain Insight for Singapore Procurement Managers: By replacing rigid plastic pails with multi-layer Bag-in-Box formats, Singaporean food manufacturing facilities typically reduce warehouse floor utilization by up to 85% for raw material packaging inventory, while lowering total carbon footprint per liquid liter transported across the Causeway or through PSA Singapore terminals by 40% to 65%.
The success of Bag-in-Box packaging in tropical Southeast Asian climates depends on film barrier performance and sealing physics. Singapore experiences sustained high ambient temperatures (30°C–34°C) and high humidity (80%–95% RH). Under these conditions, standard single-layer polyethylene bags suffer from oxygen permeation, leading to premature rancidity of edible oils, flavor degradation in beverage syrups, and spoilage of liquid dairy products.
Our engineered Bag-in-Box solutions utilize advanced co-extruded and laminated flexible barrier films engineered to maintain product integrity over extended ambient or cold-chain shelf lives:
From central kitchens supplying hawker centers to multinational pharmaceutical manufacturing in Tuas Biomedical Park.
Supplying 5L, 10L, and 20L BIB bags with universal quick-connect valves for soft drink dispensers, bubble tea chains, and institutional catering across Orchard Road and Marina Bay hospitality hubs.
Heavy-duty barrier bags designed for palm olein, sesame oil, and concentrated coconut milk used by central manufacturing kitchens in Senoko and Mandai serving Singapore's retail grocery market.
Aseptic cold-chain BIB solutions (3L to 1000L IBC liners) providing extended shelf life without preservatives, fully compatible with Jurong Cold Stores infrastructure.
Grease-proof, high-burst strength bags paired with custom outer boxes for chili sauce, soy sauce, and soup stocks supplied to HORECA central commissaries.
UN-certified industrial Bag-in-Box options for water-based chemicals, commercial cleaning agents, and liquid fertilizers utilized in Jurong Island chemical operations.
Gamma-irradiated, sterile single-use liquid processing bags and outer protective cartons for bioprocessing plants in Tuas Biomedical Park.
An objective comparison based on Singapore industrial operating metrics: storage cost per sq. meter, freight efficiency, and sustainability compliance.
| Evaluation Parameter | Bag-In-Box (BIB) System | Rigid HDPE Jerrycans (20L) | Steel / Tin Drums (200L) |
|---|---|---|---|
| Inbound Freight Volume | Optimal (Flat-Packed) | Poor (Bulky Empty Shipping) | Poor (Requires Full Container Loads) |
| Singapore Warehouse Footprint | 85% Space Reduction | High Warehousing Overhead | High Floor Loading Stress |
| Dispensing Air Ingress | Zero Air Ingress (Bag Collapses) | Air Enters (Accelerates Oxidation) | Requires Pump & Venting |
| Residual Product Waste | < 0.5% Remaining | 3% to 5% Trapped in Corners | 2% to 4% Residual Sludge |
| NEA Packaging Reporting Mandate | High Fiber Content (Easy Compliance) | Heavy Virgin Plastic Levy Impact | Complex Recycling Disposal |
| Humidity Crushing Defense | High-ECT Water-Resistant Board | Polymer Creep Under Heat | Denting / External Corrosion Risk |
In accordance with Singapore’s Ministry of Sustainability and the Environment (MSE), commercial brand owners and packaging importers in Singapore face escalating scrutiny under the Mandatory Packaging Reporting (MPR) framework governed by the National Environment Agency (NEA). Companies carrying specified turnover thresholds must annually track, report, and reduce the weight of virgin plastic packaging introduced into the domestic market.
Transitioning from rigid plastic pails and jerrycans to our fiber-first Bag-in-Box system provides an immediate baseline reduction in structural plastic usage of up to 75%. The outer protective box is manufactured from FSC-certified recyclable corrugated paperboard, which integrates seamlessly into Singapore's commercial paper recycling streams handled by NEA-licensed waste management operators.
A primary failure point for expanding food manufacturing facilities in Singapore is the disconnect between packaging material suppliers and equipment manufacturers. As an integrated packaging and machinery solutions provider (NYSE: GPK heritage), we supply not only the flexible bags and outer cartons but also high-precision, automated packaging machinery systems engineered to operate harmoniously.
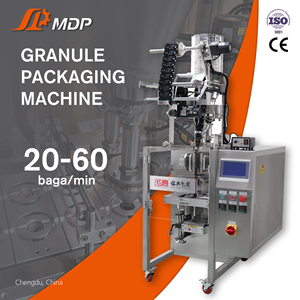
Semi-automatic single-head fillers to fully automatic continuous WEB filling systems offering high accuracy electromagnetic flow meters, CIP (Clean-in-Place) sanitation loops, and nitrogen flushing capabilities for oxygen-sensitive liquids.
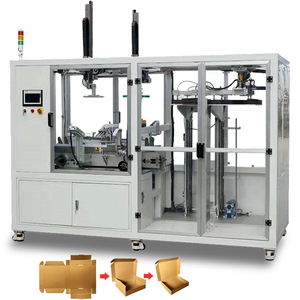
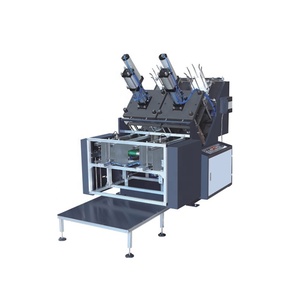
Compact footprint outer corrugated box formers, tray formers, and automatic carton sealers designed specifically for tight cleanroom and central kitchen layouts in Singapore industrial parks.
Robotic bag loading and automated tap insertion units that eliminate manual handling, reducing labor costs while maximizing hygiene compliance under SFA standards.
Demonstrated global manufacturing capacity, stringent quality control benchmarks, and dedicated regional export support.
Our manufacturing sites operate under strict global GFSI-recognized food safety standard certifications, guaranteeing complete cleanroom production and lot-to-lot traceability for food-contact liquid packaging.
Streamlined shipping routes directly into Jurong Port and PSA Tanjong Pagar / Tuas Terminals, supported by dedicated freight management teams familiar with Singapore Customs clearance procedures and GST documentation.
In-house structural design labs capable of engineering custom box geometries, drop-test verified high-ECT corrugated outer cases, and proprietary dispensing fitments matching your exact filling line parameters.
Addressing common procurement, technical, and regulatory questions regarding Bag-in-Box imports into Singapore.
Yes. All food-contact flexible inner bags and fitments are manufactured from virgin food-grade resins fully compliant with SFA food hygiene regulations, FDA 21 CFR regulations, and EU Regulation (EU) No 10/2011. Full Migration Test Certificates and Certificates of Analysis (CoA) are supplied with every export shipment.
We engineer outer boxes using high-ECT (Edge Crush Test) heavy-duty virgin kraft fluting combined with specialized moisture-resistant water-based barrier coatings. This prevents humidity degradation and box-bulging during prolonged storage in non-climate-controlled Singapore warehouses or cold storage facilities.
We manufacture standard liquid capacities including 1.5L, 3L, 5L, 10L, 20L, and 25L for commercial packaging, as well as 220L drum liners and 1000L IBC intermediate bulk container liners for industrial chemical and bulk food processing applications.
Absolutely. We offer high-definition flexographic and offset printing up to 8 colors, incorporating GS1 Singapore compliant barcodes, custom branding graphics, regulatory iconography, and localized multilingual usage instructions.
Standard export orders ship directly to PSA Singapore terminals within 14 to 21 working days from production approval. We also offer buffer stock stocking agreements for high-volume recurring enterprise clients to ensure immediate port-side dispatch.
Yes. Our bags feature industry-standard fitment options—including Vitop® taps, QCD quick-connect valves, and screw caps—making them 100% compatible with existing beverage fountain machines, commercial oil pumps, and central kitchen dispensing rigs across Singapore.
Consult with our senior packaging engineers to review your liquid product specifications, request complimentary sample kits, or obtain a comprehensive FOB / CIF Singapore port quotation today.