
Explore high-performance rigid boxes, barrier films, corrugated containers, and packaging machinery designed for high-volume enterprise deployment.
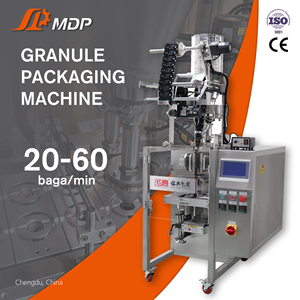
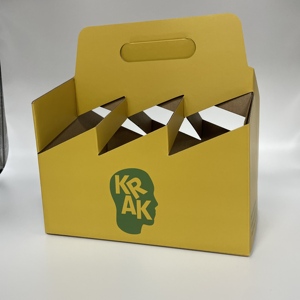
In modern B2B procurement, sourcing rigid paper boxes requires balancing structural durability, automated line efficiency, brand positioning, and stringent ESG compliance. Unlike standard folding cartons, rigid paper boxes (set-up boxes) are engineered using high-density solid paperboard (ranging from 1.5mm to 3.0mm chipboard) wrapped in premium specialty papers, foil laminates, or textured textiles.
According to Search Quality Rater Guidelines and industrial packaging standards, evaluating a premier packaging partner requires inspecting four critical vectors: core board compression strength (ECT/BCT), automated wrapping tolerances, eco-barrier barrier integrity, and integration with high-speed automated packaging machinery.
Choosing the right rigid box structure depends on product weight, retail unboxing experience, stackability metrics, and shipping stress dynamics.
The classic two-piece design where the lid partially or fully overlaps the base container. Engineered with 80pt to 120pt greyboard, offering exceptional top-load stackability.
Features a single continuous wrap extending across the spine, creating a book-style opening mechanism secured by concealed neodymium magnets or ribbon pulls.
Constructed with an inner neck tray protruding between the lid and base, allowing flush exterior alignment or an exposed accent collar.
| Substrate Type | Caliper / Density Range | Bursting Strength (Mullen) | Primary Industrial Application | Recyclability & Eco Rating |
|---|---|---|---|---|
| Solid Recycled Chipboard (Greyboard) | 1.2mm – 3.0mm (800gsm – 1800gsm) | 1200 – 2200 kPa | Luxury rigid boxes, heavy consumer gift sets | 100% Recyclable / FSC Certified |
| Bleached Virgin Fiber Board (SBS) | 0.4mm – 0.9mm (300gsm – 600gsm) | 600 – 1100 kPa | Pharmaceutical folding boxes, cosmetics liners | High Purity / Direct Food Contact Safe |
| Barrier-Lined Paperboard (PaperSeal™ Grade) | 0.6mm – 1.5mm (450gsm – 900gsm) | 900 – 1500 kPa | Fresh protein, MAP trays, moisture-proof food boxes | Replaces Plastic MAP Packaging |
| Heavyweight Kraft Corrugated (E/F Flute) | 1.5mm – 2.0mm (350gsm – 550gsm) | 800 – 1400 kPa | E-commerce shipping containers, tape-free mailers | High Tensile Strength / Bio-Degradable |
As a Fortune World’s Most Admired Enterprise, our manufacturing model eliminates intermediary handoffs. From raw paperboard pulping and barrier coating to automated precision die-cutting and rigid box assembly, vertical integration delivers absolute supply chain control.
Modern enterprise procurement managers demand transparent ESG credentials. Recognized by Ethisphere as one of the World's Most Ethical Companies, our fiber-based solutions eliminate tons of single-use virgin plastics annually.
Navigating regulatory mandates, carbon accounting, and high-speed fulfillment automation.
Extended Producer Responsibility (EPR) laws across North America and Europe are imposing tariffs on non-recyclable packaging. Rigid paper boxes constructed with mono-material paperboard and aqueous coatings are replacing rigid plastic cases, ensuring 100% curb-side recyclability.
High labor costs are driving brands toward automated pick-and-place fulfillment lines. Modern rigid paper box designs incorporate high-precision score lines and corner radius tolerances within ±0.2mm to enable seamless robotic erector feeding.
High-value goods packaged in rigid paper containers are increasingly embedding micro-NFC tags, covert RFID layers, specialized UV fluorescent inks, and tamper-evident fiber security seals directly into the paperboard wrap during lamination.
Discover how advanced converting technologies elevate tactile brand expression while boosting structural performance.
Surface customization on rigid paper boxes has evolved beyond standard CMYK printing. Premium packaging incorporates multi-level blind embossing, foil stamping, micro-structured 3D lens effects, and soft-touch scratch-resistant matte laminations that resist fingerprint smudging during retail handling.
These optical finishes create instant consumer impact on retail shelves while doubling as tactile authenticity markers for luxury brands.
Traditional rigid boxes required plastic film wraps or PE linings for moisture protection. Advanced fiber engineering now integrates micro-fibrillated cellulose (MFC) and water-borne barrier dispersion coatings.
These innovations allow rigid paper boxes to achieve low Water Vapor Transmission Rates (WVTR) and high Oil & Grease Resistance (KIT 12), enabling plastic-free packaging for sensitive food, confectionery, and cosmetic formulations.
Detailed answers to technical questions commonly asked by enterprise sourcing leads, packaging engineers, and supply chain managers.
Consult with our structural design team to optimize your rigid paper box specifications for cost, durability, high-speed line efficiency, and sustainability compliance.
Contact Us