
Explore our industrial-grade, recyclable, and precision-engineered fiber packaging line. Manufactured under international quality standards (FSC, ISO 9001, BRCGS) for global export.
Navigating regulatory mandates, plastic substitution, and operational efficiency through advanced paperboard chemistry and integrated high-speed converting machinery.
In an era defined by global regulatory shifts, strict ESG (Environmental, Social, and Governance) compliance mandates, and accelerating consumer demand for eco-conscious brand delivery, packaging is no longer merely a protective shell. It is a core strategic lever for multinational brand value, logistical risk reduction, and decarbonization. As a premier custom paperboard packaging manufacturer and exporter, Graphic Packaging International operates at the intersection of raw fiber science, advanced aqueous barrier technology, high-definition structural printing, and high-speed automated packaging machinery.
Consolidated under public financial reporting standards (NYSE: GPK) and repeatedly validated by elite corporate benchmark rankings—including Fortune World’s Most Admired Companies 2026, Ethisphere World’s Most Ethical Companies 2026, JUST Capital Best of American Business 2026, and 3BL 100 Best Corporate Citizens 2026—our enterprise platform delivers verifiable supply chain accountability. From virgin and recycled paperboard mills to fully integrated converting facilities and automated machinery systems across North America, Europe, and Asia-Pacific, we provide international procurement teams with a fully audited, single-source manufacturing infrastructure.
Balancing four fundamental metrics every procurement and brand management executive measures daily: Consumer Experience, Environmental Performance, Brand Distinction, and Total Operational Cost.
We manufacture Solid Bleached Sulfate (SBS), Coated Unbleached Kraft (CUK), and Coated Recycled Board (CRB) optimized with proprietary bio-polymer water-based barrier coatings. Our material formulations replace traditional PE, PFAS, and aluminum foil laminates while maintaining zero-grease penetration (Kit 12 compliance) and high moisture vapor transmission rate (MVTR) resistance for sensitive food products.
Our patented product platforms—such as KeelClip™ (replacing plastic multi-pack shrink wrap and rings), PaperSeal™ (replacing high-barrier MAP plastic trays for fresh meat and produce), and Boardio™ (rigid paperboard canister systems replacing tin cans and rigid plastic containers)—reduce plastic usage by up to 80-100% per unit.
Engineered compliance solutions like CleanClose™ with ChildBlock™ are certified child-resistant under 16 CFR § 1700.20 for household unit doses (detergent pods, pharmaceuticals). This structural breakthrough ensures maximum child protection while preserving easy, intuitive access for elderly consumers without requiring single-use plastic latches.
We design, manufacture, and service automated packaging machinery—including Autoflex™ basket carriers, KeelClip™ 1600, QuikFlex™, and Marksman™ SB sleeve wrappers. Designing paperboard structures and packaging machinery in tandem guarantees zero line-speed degradation and optimal operational overall equipment effectiveness (OEE).
Elevate shelf performance while mitigating counterfeit risk. Our converting facilities support multi-color flexographic and offset printing, 3D Fresnel lens technology, holographic foils, tactile embossing, micro-perforated tamper evidence, UV structural varnishes, and serialized digital watermarking for track-and-trace logistics.
With a strategic manufacturing footprint across key export regions, we provide global supply security. Our fiber sources are certified under FSC® (Forest Stewardship Council), PEFC™, and SFI® standards, ensuring complete compliance with the European Union Packaging and Packaging Waste Regulation (PPWR) and global Extended Producer Responsibility (EPR) frameworks.
Key structural disruptions shaping global FMCG, retail, and food service packaging specs over the next decade.
Global packaging procurement is undergoing its most radical transformation since the advent of industrial polymers. Procurement directors and packaging engineering teams must align structural design with aggressive global decarbonization targets, regulatory bans on single-use plastics, and volatile freight economics. Based on market intelligence compiled across enterprise supply chains, four macro trends dominate future sourcing strategies:
The European Union Packaging and Packaging Waste Regulation (PPWR) has established strict design-for-recycling (DfR) benchmarks. By 2030, all packaging circulating within the EU market must be fully recyclable at scale (Design Grade A or B). International exporters shipping consumer goods into European or North American markets are actively phasing out complex multi-layer plastic-laminated paperboards in favor of aqueous-coated, mono-material paper structures. Sourcing teams are shifting specifications toward repulpable paperboard options that easily pass standard PTS and Western Michigan University (WMU) recycling protocols.
Secondary packaging in the beverage, canned food, and personal care sectors is rapidly eliminating secondary shrink film and plastic ring carriers. Driven by retail mandates (such as Walmart’s Project Gigaton and major European grocery chain policies), brand owners are adopting paperboard clip systems like KeelClip™ and enclosed corrugated mailer solutions. These fiber alternatives not only remove soft plastic waste from ocean and landfill streams but also unlock 360-degree high-definition print area for primary brand messaging right on the retail shelf.
In fresh protein, ready-to-eat meals, and fresh agricultural produce, Modified Atmosphere Packaging (MAP) has historically relied on heavy CPET, APET, or polypropylene tray structures. Next-generation paperboard tray technology, exemplified by PaperSeal™, utilizes a precision-formed paperboard tray lined with an ultra-thin barrier film that can be cleanly separated by the end consumer prior to paper recycling. This achieves an instant 80% reduction in plastic resin usage per package while maintaining essential shelf-life gas barrier integrity (O2 and CO2 retention).
B2B buyers are moving away from fragmented sourcing models where paperboard substrates, converting plants, and line machinery come from separate third-party vendors. Multi-vendor friction frequently results in downtime during seasonal volume surges due to minor caliper variances or glue-flap misalignments. Future-focused procurement strategies favor single-source partners who engineer both the paperboard structural converting and the automated high-speed cartoners or sleeve wrappers, ensuring total operational accountability and guaranteed overall equipment effectiveness (OEE).
How custom paperboard formulations are pushing performance boundaries across temperature, moisture, and mechanical stress profiles.
Replacing traditional polyethylene extrusion coatings with dispersion-coated water-based barriers allows paperboard to remain repulpable in standard paper mill recovery systems. These dispersion layers provide exceptional oil, grease, and moisture resistance for takeaway salad bowls, greaseproof sandwich wraps, and frozen food cartons.
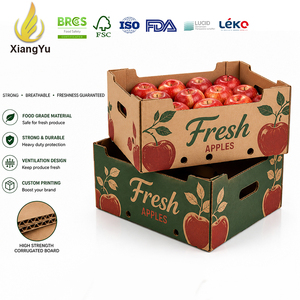
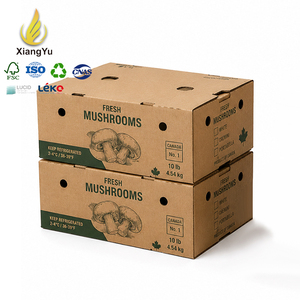
Fresh produce export demands precise thermodynamic airflow and moisture regulation. Advanced structural engineering integrates custom ventilation die-cuts with water-resistant kraft liners (hydrophobic sizing), preventing box softening under high-humidity cold-chain transport (0°C to 4°C at 95% RH) while protecting apples, mushrooms, and fresh berries from compression damage.
Modern paperboard converting integrates invisible digital watermarks (e.g., Digimarc) and serialized dynamic 2D barcodes into graphic layouts. This enables rapid cashier scanning, automated warehouse sorting, anti-counterfeiting verification for luxury or pharmaceutical items, and direct consumer engagement through smartphone scanning.
From initial technical audit to commercial-scale automated line integration, our engineering process de-risks every packaging transition.
Technical review of your product metrics, retail distribution channels, volume targets, barrier specs, and existing line machinery.
CAD structural engineering, 3D digital proofing, rapid physical sampling, and FEA load testing for burst and edge-crush performance.
Matching exact paperboard fiber grades (SBS, CUK, CRB), barrier dispersions, and eco-friendly printing ink systems to your target compliance market.
Validation trials on your existing packaging lines or co-engineering dedicated high-speed machinery systems for flawless cartoning performance.
Commercial production manufacturing across localized converting plants backed by continuous technical service support.
Expert answers to technical, regulatory, material, and logistics queries for international procurement teams.
Connect with our global technical team to request custom structural samples, discuss barrier requirements, or review high-speed machinery integration for your enterprise.