
Standardized and custom-engineered corrugated boxes, rigid display containers, and barrier-coated export packaging built to ISO 9001 & FSC certified manufacturing standards.
As global brands transition away from single-use plastics under stringently enforced environmental mandates—such as the European Union Packaging and Packaging Waste Regulation (PPWR) and US State-level Extended Producer Responsibility (EPR) laws—corrugated board has evolved from a simple transport shell into a highly engineered, high-performance structural barrier platform.
As a leading China corrugated packaging boxes manufacturer and global exporter, our engineering facilities utilize advanced multi-layer paperboard fluting technology combined with sustainable aqueous barrier coatings. This technical whitepaper explores how optimized flute profiles, high-ECT (Edge Crush Test) liners, and automated line compatibility deliver optimal cost efficiency, structural safety, and brand elevation for international procurement officers.
Selecting the precise corrugated flute profile is critical to balancing compression strength, stacking capacity, cushion protection, and ocean freight volume efficiency. Our production lines integrate single-wall and double-wall combinations customized for specific product densities:
Thickness: 1.1mm – 1.6mm | 90 Flutes/ft
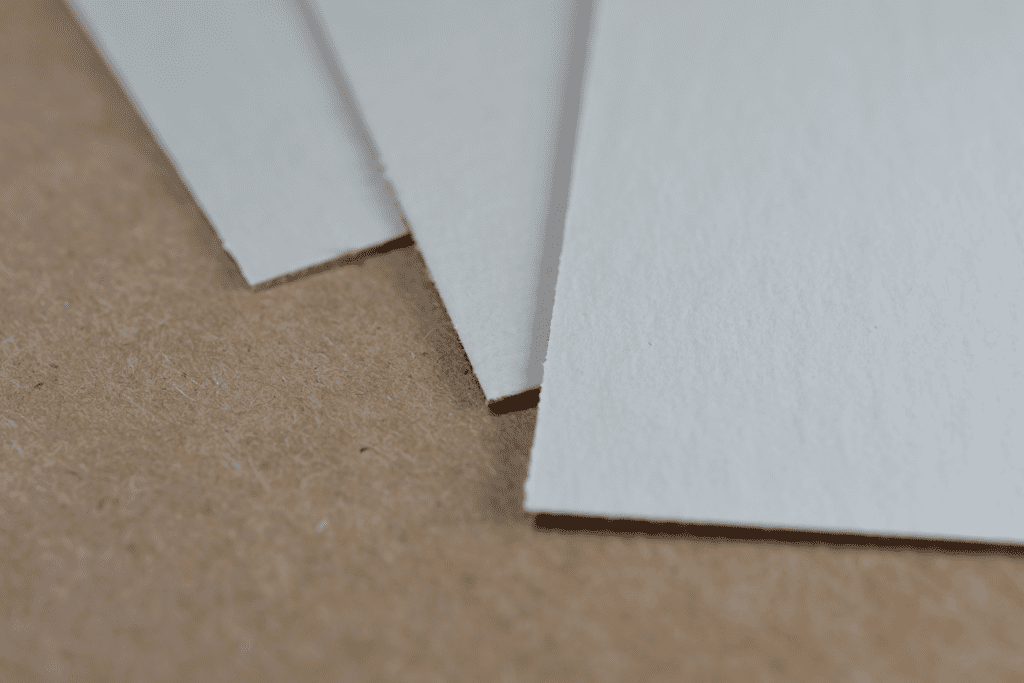
Designed for premium retail folding cartons, cosmetic boxes, and direct-to-consumer mailers. Provides a smooth outer liner for high-definition offset printing, hot foil stamping, and tactile spot UV finishes.
Thickness: 2.5mm – 4.0mm | 39–49 Flutes/ft
The global benchmark for beverage multipacks, vented fresh produce containers, and consumer goods. Offers balanced puncture resistance and stacking strength for multi-tier pallet transportation.
Thickness: 4.5mm – 6.8mm | Heavy-Duty
Engineered for high-gross-weight industrial exports, medical equipment shipping, red wine 12-pack dividers, and bulk agricultural distribution requiring severe stacking humidity resistance.
Modern global logistics require strict adherence to international shipping container standards. While traditional Mullen Bursting Strength tests measure the pressure required to puncture a box wall (expressed in lbs per sq. inch), modern automated supply chains focus on Edge Crush Test (ECT) values, which measure top-to-bottom compression strength—the decisive factor in pallet stacking safety.
Our OEM manufacturing facilities utilize high-yield virgin kraftliners (up to 440g/m²) combined with semi-chemical fluting medium to achieve maximum stacking stability under high relative humidity (RH 85%+) during ocean freight journeys from Asian ports to European and North American distribution centers.
Combining vertical paperboard manufacturing, automated structural converting, high-speed machinery integration, and audited global compliance.
Unlike third-party packagers or trading intermediaries, our China manufacturing hubs operate fully integrated converting lines. We control paperboard slitting, corrugated fluting, multi-color flexographic and offset printing, rotary die-cutting, structural partition insertion, and automated gluing under one quality control system.
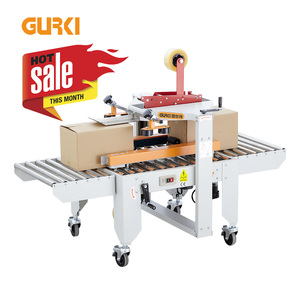
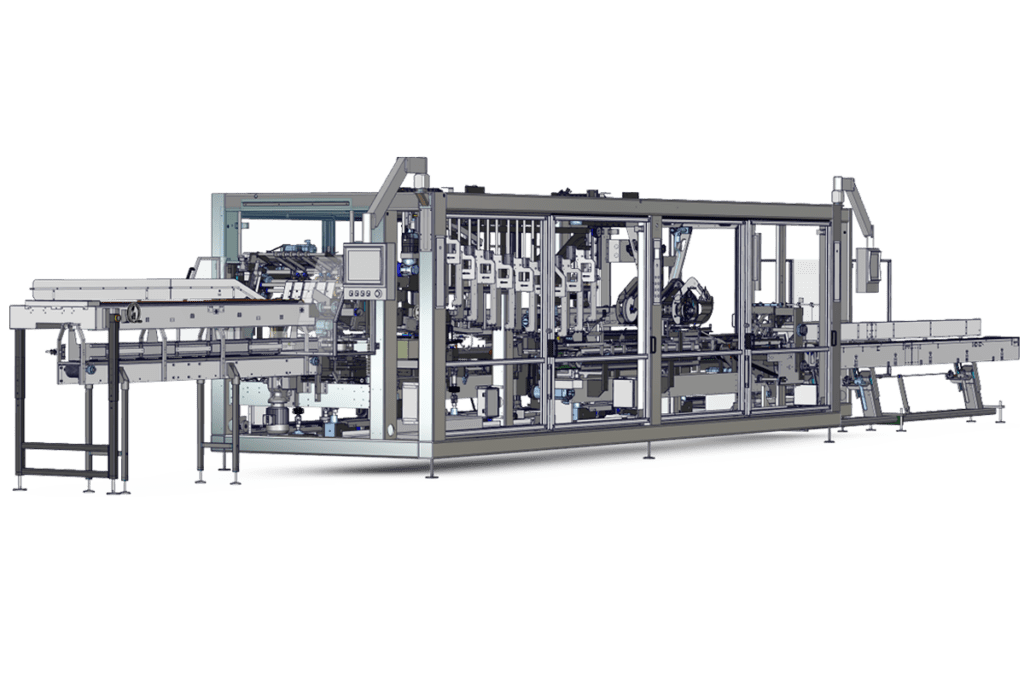
Packaging failure often occurs not from poor board quality, but from misalignment between box specifications and high-speed automated packaging machinery. We engineer packaging boxes alongside case sealers, cartoning systems, and automated taping lines (such as GURKI auto case sealers) to guarantee flawless line speeds.
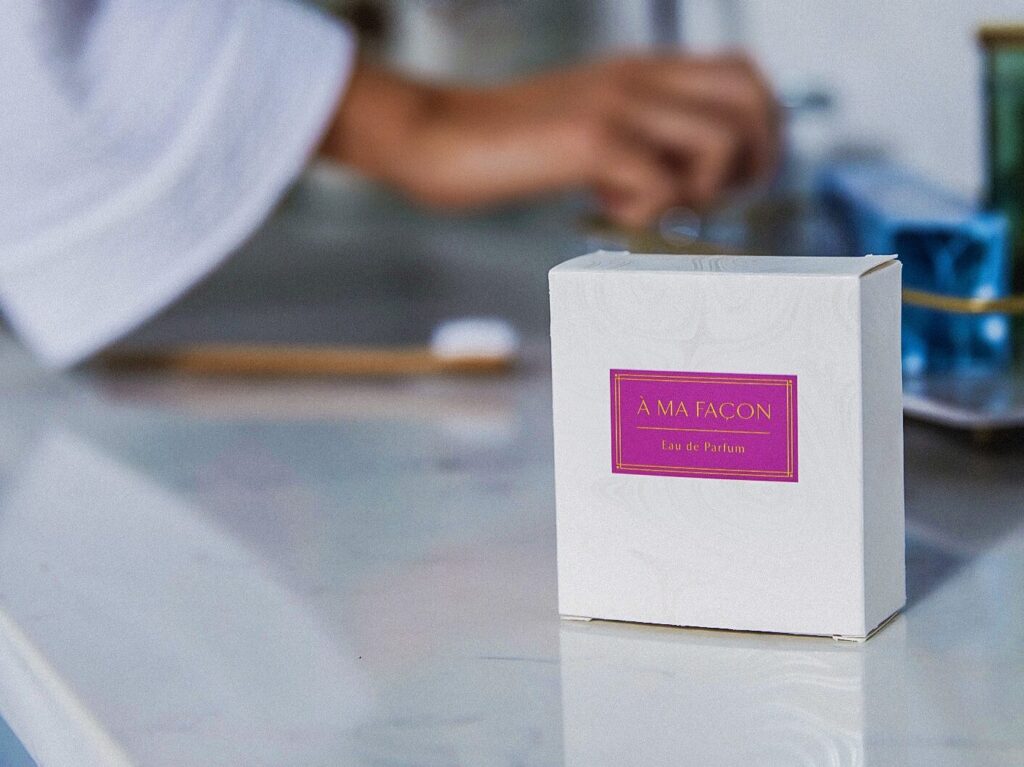
Packaging is the primary physical touchpoint between your brand and the consumer. Our facility houses 8-color Heidelberg offset presses, high-speed flexo printer slotters, micro-embossing tools, and gold/silver foil stamping machinery designed to make products stand out on crowded retail shelves.
Global procurement leaders in beverage, fresh food, consumer electronics, and e-commerce must navigate rapid market shifts driven by sustainability mandates, supply chain digitizations, and freight cost optimization.
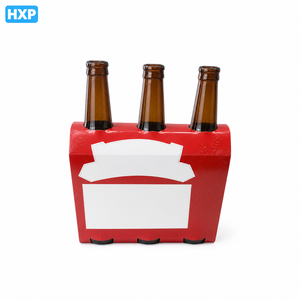
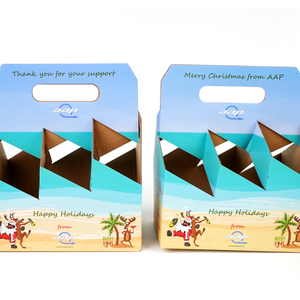
Global beverage giants are systematically replacing plastic ring carriers and PVC shrink film with 100% recyclable paperboard clip-style multipacks (such as KeelClip™ style solutions) and heavy-duty basket carriers. Our factory provides automated flat-pack multipacks that reduce plastic reliance to zero while offering 360-degree brand graphic real estate.
With the rise of bio-based coatings, paperboard trays with removable barrier liners (such as PaperSeal™ technologies) are replacing traditional rigid plastic Modified Atmosphere Packaging (MAP) trays for fresh protein, produce, and bakery products, cutting plastic consumption by up to 80% per unit.
Freight costs are directly linked to volumetric weight. Modern corrugated manufacturing utilizes micro-fluting and high-yield recycled testliners treated with strength-enhancing starches, maintaining high ECT ratings while reducing overall package weight by 12% to 18%.
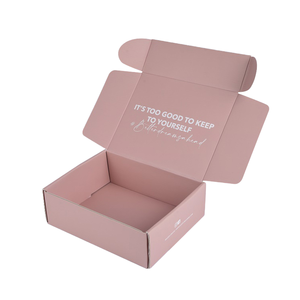
Direct-to-consumer (D2C) brands require tamper-evident corrugated mailers with self-sealing adhesive strips and tear-strip openers. Custom internal corrugated dividers replace plastic bubble wrap, streamlining fulfillment times and reducing dimensional weight (DIM weight) penalties.
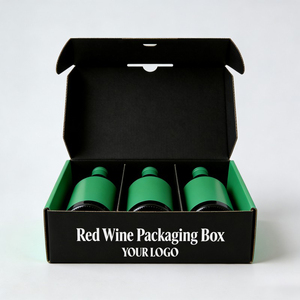
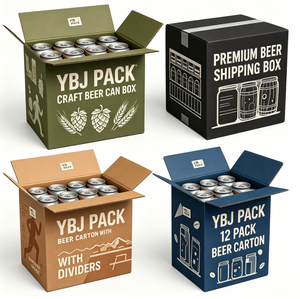
Glass bottles and metal cans demand maximum impact absorption during transit. Our 3-bottle, 6-bottle, and 12-bottle beverage shipping containers integrate pre-assembled corrugated cell dividers. Engineered with thick double-wall board, these boxes prevent bottle-to-bottle contact and withstand vertical drop forces during export logistics.
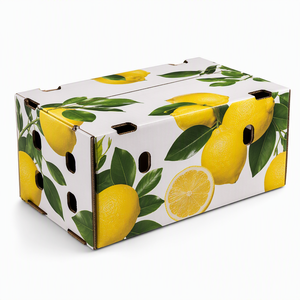
Request Beverage SpecsExporting fresh citrus, lemons, and delicate produce requires containers that facilitate air movement during cold-chain storage while retaining stacking strength in high-humidity environments. Our vented corrugated agricultural boxes feature precision die-cut air channels and water-resistant wax or aqueous coatings.
Request Agricultural Specs
Expert answers to common commercial, engineering, and logistics questions from international buyers, sourcing agents, and OEM procurement managers.