
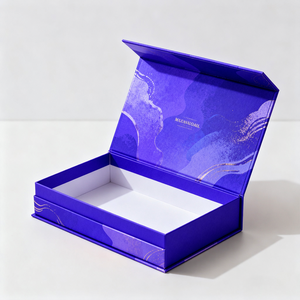
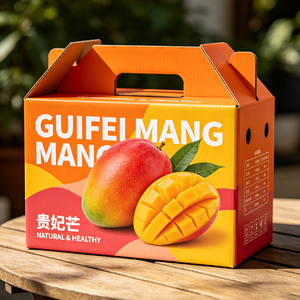
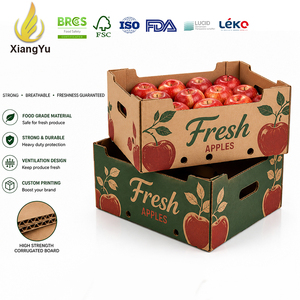
Explore our engineered paperboard multipacks, rigid fruit cartons, barrier-lined trays, and custom protective corrugated mailers manufactured to rigorous global specifications.
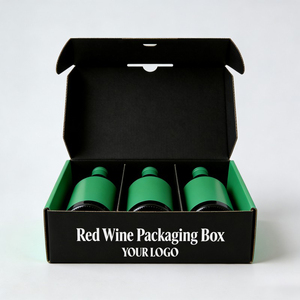
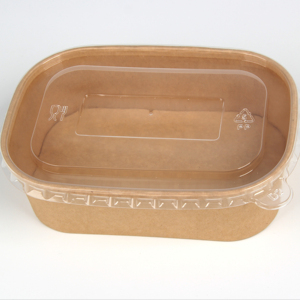
The global beverage packaging sector is undergoing a profound structural evolution. Procurement executives, supply chain directors, and packaging engineers face escalating regulatory pressures—such as the European Union’s Single-Use Plastics Directive (SUPD) and expanding extended producer responsibility (EPR) legislation across North America. As brands systematically sunset traditional plastic hi-cone ring carriers and shrink-wrap films, China wholesale can carrier packaging factories have established themselves as pivotal engineering powerhouses for paperboard and fiber-based alternatives.
Transitioning from plastic rings to paperboard clip-style multipacks (such as top-clip, keel-style, basket carriers, and fully enclosed wrap-around cartons) requires far more than replacing raw substrate. It demands a holistic re-engineering of wet-strength fiberboard, high-speed automated cartoning machinery alignment, precision structural die-cutting, and structural stress management under cold-chain moisture conditions.
Specially formulated Unbleached Kraft (CUK) and Solid Bleached Sulfate (SBS) substrates treated with water-resistant sizing to ensure zero carrier failure in high-humidity cold storage and ice-chest environments.
Precision tolerance (+/- 0.2mm) top-clip aperture cuts designed to seamless integrate with high-speed multipack cartoning equipment like AutoMaxx, QuikFlex, and Marksman SB lines.
Engineered finger-apertures and reinforced handle structures offering superior consumer carry comfort, enhanced billboarding surface area, and maximum shelf appeal.
Compare mechanical properties, line speeds, and sustainability scores across major wholesale fiber packaging formats manufactured in OEM/ODM Chinese facilities.
| Format Type | Primary Material Substrate | Cobb Value (Water Abs.) | Bursting Strength (KPa) | Automated Line Speed | EPR/Recyclability Rating |
|---|---|---|---|---|---|
| Clip-Style Top Carrier (Keel-Style) | Carrier Kraft (CUK) / 300-450 GSM | < 30 g/m² (Cobb 30) | > 1800 KPa | Up to 400 Cans/Min | 100% Curbside Recyclable |
| Basket Carrier Multipack | High-Grammage SBS / Coated Kraft | < 35 g/m² | > 2100 KPa | Up to 250 Units/Min | 100% Paper Recyclable |
| Wrap-Style Enclosed Carton | Corrugated B-Flute / Micro-Flute F | < 40 g/m² | > 2400 KPa | Up to 300 Packs/Min | High Recyclability |
| Barrier-Lined Produce Trays | Paperboard + Bio-Lamination | < 15 g/m² | > 1600 KPa | Manual / Semi-Auto | Compostable / Recyclable |
| Rigid Magnetic Shipping Mailer | Grayboard + Coated Cardboard | Standard Moisture Proof | > 3500 KPa | Hand-Assembly / Custom | Premium Reusable Format |
Leveraging integrated pulp-to-converter manufacturing, certified ESG compliance, and end-to-end quality assurance for global beverage brands.
Our raw paperboard is strictly sourced from responsibly managed forests certified under FSC and PEFC standards. We guarantee zero illegal deforestation fiber across all product lines.
We solve the "carton-machine disconnect." Our structural engineering team tests every clip and multipack sleeve against high-speed automated cartoning systems to prevent line jams and tear failures.
Aligned with Fortune Most Admired and Ethisphere World's Most Ethical standards, our state-of-the-art Chinese plants undergo rigorous SEDEX SMETA and BSCI third-party labor and environmental audits annually.
From CAD structural dielines to sample delivery in as little as 72 hours. We utilize advanced 3D visual proofing and digital sample cutting to accelerate your product time-to-market.
Offerings include food-safe aqueous coatings, soft-touch matte lamination, spot UV, holographic security foils, and anti-counterfeit micro-printing for brand protection.
By streamlining raw material procurement, optimizing pallet load density, and maintaining high manufacturing efficiencies, we offer international buyers competitive tier-1 wholesale pricing.
As global brands set aggressive 2025 and 2030 ESG milestones, procurement managers must anticipate technological advancements and regulatory shifts in beverage multipack sourcing. The following four macro-trends are reshaping factory specifications across China and global manufacturing hubs:
Traditional paperboard carriers often relied on thin PE film laminations for moisture resistance. Future sourcing focuses on plastic-free, water-based dispersion barrier coatings that allow paperboard multipacks to be repulped easily in standard paper recycling mills without microplastic contamination.
Driven by raw material cost optimization and carbon footprint reduction, factories are using micro-flute corrugated structures (such as F-flute and N-flute) and high-density virgin fiber blends. This maintains bursting strength while reducing overall packaging weight by 12% to 18%.
High-volume can carrier packaging is increasingly featuring laser-etched matrix codes, variable data QR codes, and invisible anti-counterfeiting marks. This allows beverage brands to track batch supply chains, run consumer engagement campaigns, and combat gray-market diversion.
Global co-packers and contract manufacturers demand paperboard clips that function seamlessly across multiple machine brands. Chinese suppliers are standardizing die-cut specifications to ensure plug-and-play operation across European and American cartoning lines.
Detailed answers to critical technical, logistical, and commercial queries from international buyers and packaging engineers.
Upgrade your beverage portfolio with eco-friendly paperboard clips, high-strength fruit cartons, and automated machine-compatible multipacks. Request engineered samples and wholesale factory pricing today.