CE Certified & Food Safety Compliant

CE Certified Produce Packaging Boxes Manufacturers & Exporters

Engineering High-Performance Corrugated Cartons, Ventilated Export Trays & Sustainable Cold-Chain Packaging Solutions for Global Fresh Agriculture Markets

Export-Grade Product Portfolio

Featured Fresh Produce Packaging Cartons

Standardized and custom-designed corrugated cardboard boxes equipped with engineered thermodynamic air vents, hydrophobic barrier coatings, and heavy-duty stackability for international sea & air freight.
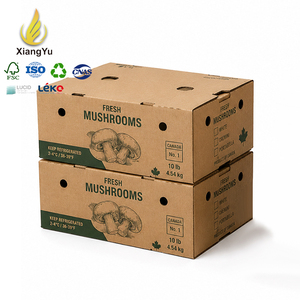
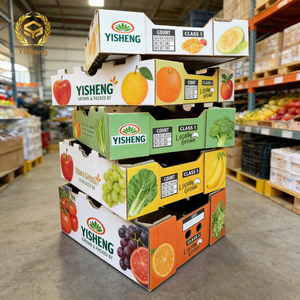
Ventilated Fresh Vegetable Mushroom Fruit Box

Manufacturer Direct Custom Printed Corrugated Cardboard Ventilated Fresh Vegetable Mushroom Fruit Wholesale Food Packaging Boxes

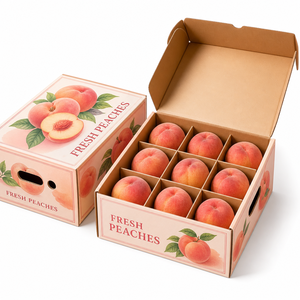
Custom Protective Peach Packaging Box

Custom Protective Peach Packaging Box Corrugated Fruit Gift Carton For Farm Retail And Fresh Produce Delivery

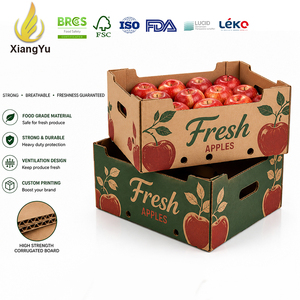
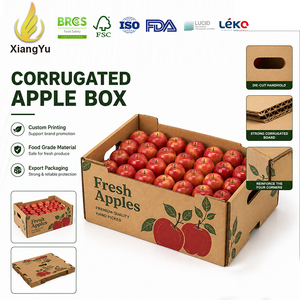
Apple Vegetable Export Packaging Box

Custom Fruit Packaging Box Corrugated Cardboard Carton for Fresh Apples Vegetables Produce Export Shipping Manufacturer

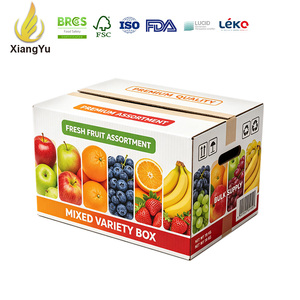
Air Hole Custom Corrugated Shipping Carton

Xiangyu Fruit Packaging Box With Air Hole Custom Corrugated Shipping Carton For Mixed Fruit Fresh Produce Export Packaging

Recyclable Breathable Corrugated Box

Recyclable Custom Printing Cardboard Fruits Vegetables Packaging Carton Breathable Corrugated Cardboard Box for Fruit

Custom Apple Packaging Box Export Supplier

Custom Apple Packaging Box Corrugated Carton For Fresh Fruit Export Transportation Agricultural Produce Packaging Supplier

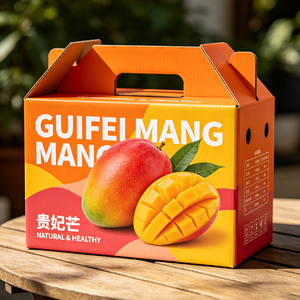
Waterproof Recyclable Mango Shipping Carton

Free Design Premium Mango Packaging Box Custom Logo Printed Waterproof Recyclable Corrugated Cardboard Fruit Shipping Carton Box

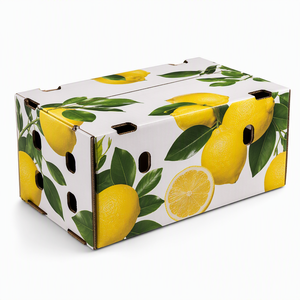
Vented Lemon Citrus Shipping Carton

Custom Printed Corrugated Lemon Packaging Box Vented Citrus Shipping Carton For Produce Export And Distribution

CE & EC
Certified Food Safety Compliance
+45%
Higher Stacking Strength under 95% RH
100%
Bio-degradable & Plastic-Free Materials
35%
Faster Forced-Air Pre-Cooling Efficiency
Industry Whitepaper & Technical Benchmark

CE Certified Agricultural Packaging: Technical Architecture for Global Supply Chains

In global fresh produce supply chains, packaging is not merely a container—it is a critical post-harvest preservation mechanism. As certified manufacturers and international exporters, we engineer corrugated paperboard solutions tailored to withstand cold-chain humidity, high compressive stacking forces, and stringent food contact regulations established by the European Union and international trade bodies.

Regulatory Compliance: CE & Food Contact Certification

Navigating export markets requires rigorous adherence to safety standards. Our produce packaging boxes undergo comprehensive testing under EU Regulation (EC) No 1935/2004 for direct food contact and Directive 94/62/EC for heavy metal concentration limits in packaging waste.

  • Heavy Metal Compliance: Combined levels of Lead (Pb), Cadmium (Cd), Mercury (Hg), and Hexavalent Chromium (Cr VI) restricted under 100 ppm.
  • Zero Harmful Migration: Aqueous, bio-based barrier coatings prevent mineral oil hydrocarbons (MOSH/MOAH) from entering fresh produce skin.
  • FSC & PEFC Traceability: 100% sourced from responsibly managed forests, supporting eco-conscious EU buyer procurement benchmarks.

Cold-Chain Moisture Integrity & Hydrophobic Coatings

High relative humidity (90% to 98% RH) inside cold storage rooms causes standard kraftliner to lose up to 60% of its structural compression within 72 hours. Our proprietary engineering counters this through hydrophobic paperboard laminations.

  • Water-Resistant Barrier (Cobb 30): Surface water absorption restricted to < 30 g/m² in 30 minutes, preventing fiber softening.
  • High-Density Kraft Fluting: Semi-chemical fluting medium enhanced with starch cross-linking resins for permanent humidity resistance.
  • Anti-Fungal Bio-Coatings: Natural organic antimicrobial treatments that minimize mold growth during multi-week ocean transit.
Engineering Specifications

Corrugated Produce Box Structural Comparison Matrix

Selecting the optimum flute combination and paperboard weight for specific agricultural crop requirements.

Produce Category Recommended Box Type Flute Profile Edge Crush Test (ECT) Box Crush Test (BCT Target) Target Cold Chain RH
Citrus & Lemons Vented Telescopic Carton (Top/Bottom) BC Double Wall (6.0mm) 14.5 - 18.0 kN/m > 9,500 N 85% - 90% RH @ 4°C - 8°C
Apples & Pears Open-Top Stackable Punnet Tray C-Flute / EB-Flute 11.0 - 14.0 kN/m > 7,800 N 90% - 95% RH @ 0°C - 2°C
Mangoes & Tropical Fruit Display Tray with Reinforced Corners B-Flute Single Wall 8.5 - 11.5 kN/m > 6,200 N 85% - 90% RH @ 12°C - 14°C
Peaches & Stone Fruit Die-Cut Gift Box with Partition Dividers E-Flute / B-Flute 7.0 - 9.5 kN/m > 4,800 N 90% RH @ 0°C - 1°C
Berries & Mushrooms High-Ventilation Shallow Punnet Outer EB Micro-Flute 9.0 - 12.0 kN/m > 5,500 N 95% RH @ 0°C - 4°C
Aerodynamic Innovation

Thermodynamic Air Vent Hole Design for Post-Harvest Longevity

Fresh fruits and vegetables are active biological organisms that continue to respire post-harvest, releasing carbon dioxide, ethylene gas, and thermal heat energy. Sub-optimal ventilation leads to heat accumulation, rapid pulp softening, and decay.

Forced-Air Cooling Optimization

Our die-cut ventilation holes are positioned in strict alignment with international pallet forced-air cooling standards. Aligning side vents across stacked pallets reduces forced-air cooling cycles by up to 35%, saving cold-storage energy costs while achieving core temperature pull-down rapidly.

Optimized Vent Ratio vs Strength

Traditional vent holes can weaken structural corners. Utilizing advanced FEA (Finite Element Analysis) modeling, our engineers shape rectangular-radius and elliptical air holes that maintain a optimal 5% to 7% vent-to-surface area ratio, preserving 92% of compression capacity.

Ethylene & Moisture Venting

Accumulated ethylene accelerates ripening and rot. Strategic top-to-bottom airflow channels inside the corrugated fluting matrix dissipate ethylene gas build-up and prevent internal condensation droplets from bruising sensitive fruit skins.

Strategic Sourcing Insights

Future Procurement & Packaging Trends in Agriculture (2025-2030)

Global fresh produce importers, supermarket chains, and farm operations are rapidly adjusting their procurement strategies to align with environmental mandates and consumer preferences.

1. EU Packaging & Packaging Waste Regulation (PPWR) Shift

With the impending EU PPWR regulations mandating significant reductions in single-use plastic punnets and micro-plastic film wraps, the market is undergoing a massive shift toward 100% fiber-based open-top corrugated trays and paperboard punnets with window die-cuts. Exporters adopting CE-certified mono-material corrugated solutions ensure uninterrupted market access across European retail chains.

2. Transition from Wax-Coated to Bio-Polymer Aqueous Barriers

Historically, produce boxes relied on paraffin wax dipping for water resistance, rendering boxes unrecyclable. Modern procurement standards mandate 100% repulpable water-based dispersion coatings. Our zero-wax formulations allow boxes to be recycled directly in standard paper mill waste streams, eliminating landfill surcharges for European importers.

3. High-Definition Flexo & Retail-Ready Packaging (RRP)

Produce packaging is transitioning from plain brown transport cartons to vibrant, shelf-ready display boxes. Utilizing high-definition water-based 6-to-8 color flexographic printing with zero volatile organic compounds (VOCs), growers can transform transit cartons directly into retail promotional units upon reaching supermarket floors.

4. Smart Packaging & Digital Traceability Integration

Modern export cartons are integrating high-density 2D matrix QR codes, GS1 Digital Links, and temperature-monitoring RFID indicators directly onto printed corrugated surfaces. This allows real-time batch tracking, farm-to-fork origin verification, and instant cold-chain compliance auditing during customs inspection.

Enterprise Manufacturing Excellence

Why Global Produce Exporters Partner with Our Manufacturing Network

Combining paperboard manufacturing, structural packaging design, high-speed automated die-cutting, and integrated machinery solutions under one certified production ecosystem.

End-to-End Vertical Integration

From virgin wood fiber pulp sourcing and high-performance linerboard corrugation to precision printing and automatic gluing, our end-to-end production control guarantees batch-to-batch structural uniformity and unyielding quality control.

High-Volume Export Scalability

Operating multi-stage corrugators capable of producing over 500,000 agricultural shipping cartons daily. We support large-scale seasonal harvesting peaks for multinational agricultural conglomerates without lead-time bottlenecks.

Rigorous QA Laboratory Testing

Every batch undergoes stringent FEFCO and ISTA standard laboratory testing: Bursting Strength (Mullen test), Ring Crush Test (RCT), Edge Crush Test (ECT), Cobb Water Absorption Test, and environmental chamber compression testing.

Need Custom Sizing or Structural Prototyping for Your Harvest Season?

Our packaging engineers provide complimentary 3D structural CAD drawings, sample prototyping, and cold-chain compression simulations tailored to your specific fruit or vegetable dimensions.

Procurement Knowledge Base

Frequently Asked Questions (FAQ)

Detailed answers regarding technical specifications, minimum order quantities, CE compliance, and international shipping protocols.

What specific certifications do your produce packaging boxes carry for export to the EU and North America?
Our produce packaging boxes are certified compliant with CE standards, EU Regulation (EC) No 1935/2004 for direct food contact safety, and EU Directive 94/62/EC for heavy metal restrictions. In addition, our manufacturing facilities hold ISO 9001 quality management, ISO 22000 / BRCGS packaging safety certifications, and FSC (Forest Stewardship Council) chain-of-custody accreditation for sustainable paperboard sourcing.
How do your corrugated fruit boxes resist collapsing during long-distance cold-chain transport?
We utilize high-density virgin kraftliner facings combined with resin-fortified semi-chemical fluting media (B-flute, C-flute, or BC double-wall). Furthermore, we apply hydrophobic water-repellent dispersion coatings (Cobb 30 rated) to both outer and inner paperboard surfaces. This prevents ambient moisture in 90%-98% RH cold storage units from softening paper fibers, ensuring high Box Crush Test (BCT) values across multi-week sea freight shipments.
Can air vent configurations be customized according to our cooling equipment?
Yes. Our structural engineering team customizes vent hole geometry, placement, and dimensions based on your specific post-harvest cooling method—whether forced-air cooling, hydro-cooling, or standard room refrigeration. Vent positions are calculated to align perfectly across standard ISO 1200x1000mm or 1200x800mm pallet layouts to maintain continuous airflow channels without degrading vertical corner stack strength.
What is the Minimum Order Quantity (MOQ) and typical lead time for custom export orders?
For custom die-cut and printed corrugated produce cartons, our standard MOQ starts at 3,000 to 5,000 units depending on box dimensions. Lead times for structural sample prototyping are 3 to 5 business days, while full-scale mass production orders are typically completed and dispatched within 12 to 18 business days from final artwork approval.
Are your produce boxes suitable for direct consumer retail display?
Absoltely. We manufacture open-top display trays, shelf-ready packaging (SRP), and gift-grade produce boxes featuring high-definition flexo or offset printing with up to 8 colors plus inline UV coating. These boxes serve dual roles: high-strength protective shipping containers during transit, and eye-catching retail displays when placed directly on supermarket shelves.
Are these corrugated produce containers 100% recyclable and plastic-free?
Yes. Unlike traditional wax-dipped boxes which cannot be processed by recycling mills, our boxes utilize advanced water-based bio-barrier coatings and water-soluble inks. They are 100% repulpable, biodegradable, and fully compliant with global circular economy legislation and plastic-reduction mandates.

Accelerate Your Produce Export Efficiency Today

Partner with an industry-leading CE certified manufacturer. Connect with our technical packaging specialists to discuss customized dimensions, cold-chain specifications, sample requests, and competitive wholesale pricing.

Contact Us