CE Certified Custom Retail Packaging Suppliers & Exporters

Sustainable Fiber-Based Solutions, High-Barrier Packaging Films & Integrated Packaging Machinery for Global Brands

Export-Grade Product Lineup

Featured Retail & Industrial Packaging Solutions

Fully compliant with European CE safety marking, EU Directive 94/62/EC, and global food-contact regulatory standards.
CE & ISO
Full EU Safety & Compliance
100%
Virgin & Recyclable Fiber Options
80+
Global Export Destinations
<0.02%
Defect Rate across Automated Lines
Industry Whitepaper Analysis

The Strategic Imperative of CE Certified Custom Packaging in Modern Global Supply Chains

In an era defined by stringent environmental directives, heightened consumer vigilance, and international supply chain complexities, retail packaging has transitioned from a basic protection vessel into a core strategic asset. Modern multi-national brand owners, FMCG manufacturers, and e-commerce conglomerates no longer source packaging based solely on unit pricing. Instead, strategic procurement hinges on CE Certification compliance, structural integrity, high-speed line compatibility, and circular economy readiness.
Industry Recognition and Global Certification Awards

Navigating European & Global Compliance Benchmarks

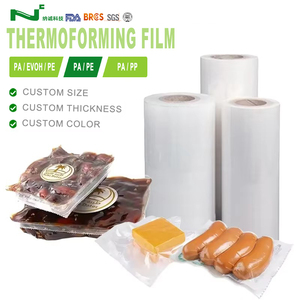
Securing CE marking and international safety conformity ensures that custom packaging meets comprehensive European health, safety, and environmental protection standards. Whether deploying multi-layer co-extruded thermoforming barrier films (such as PA/EVOH/PE structures) or heavy-duty recyclable corrugated folding cartons, regulatory alignment guarantees seamless customs clearance across the EU, North America, and Asia-Pacific markets.

  • Compliance with EU Packaging and Packaging Waste Regulation (PPWR) directives
  • Strict adherence to food-contact safety standards (FDA 21 CFR & EU 10/2011)
  • Complete traceability of raw materials from sustainable forestry (FSC/PEFC) to finished converting
  • Zero heavy-metal contamination, meeting Directive 94/62/EC threshold limits
Enterprise Distinction

Why Industry Leaders Select Our Packaging Ecosystem

We unite paperboard manufacturing, flexible polymer extrusion, custom converting, and automated packaging machinery engineering into one single-source platform.

Regulatory Safety & Rigorous QA

Our packaging substrates undergo rigorous laboratory testing for tensile strength, oxygen transmission rates (OTR), water vapor transmission rates (WVTR), and seal integrity. CE certification guarantees compliance with international safety protocols.

End-to-End Packaging & Machinery Alignment

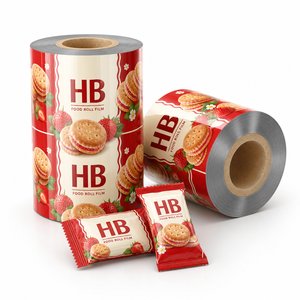
Unlike standalone converters, our custom packaging formulations—from beverage multipack carriers to thermoforming films—are specifically engineered to integrate flawlessly with automated cartoning, pick-and-place, and sleeve wrapping equipment.

Global Export & Supply Chain Resiliency

With multi-site production facilities, strategic raw material buffering, and audited ESG compliance practices, we provide multinational procurement officers with guaranteed lead times and minimized geopolitical risk.

Material Science Breakthroughs

High-Barrier Flexible Packaging & Eco-Friendly Substrates

The retail industry is undergoing a dual shift: eliminating unnecessary single-use plastics while simultaneously maximizing product shelf life to mitigate global food waste. Our advanced PA/EVOH/PE thermoforming base webs and PVDC composite hard films provide absolute barriers against oxygen, aroma migration, and moisture ingress.

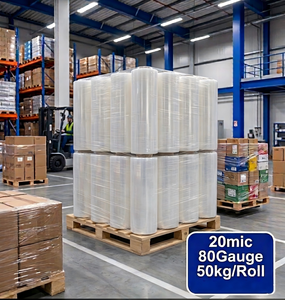
Conversely, for e-commerce and retail dry goods, our custom engineered folding cartons and high-gauge LLDPE jumbo stretch wraps deliver superior puncture resistance and structural rigidity during transit, lowering overall total cost of ownership (TCO).
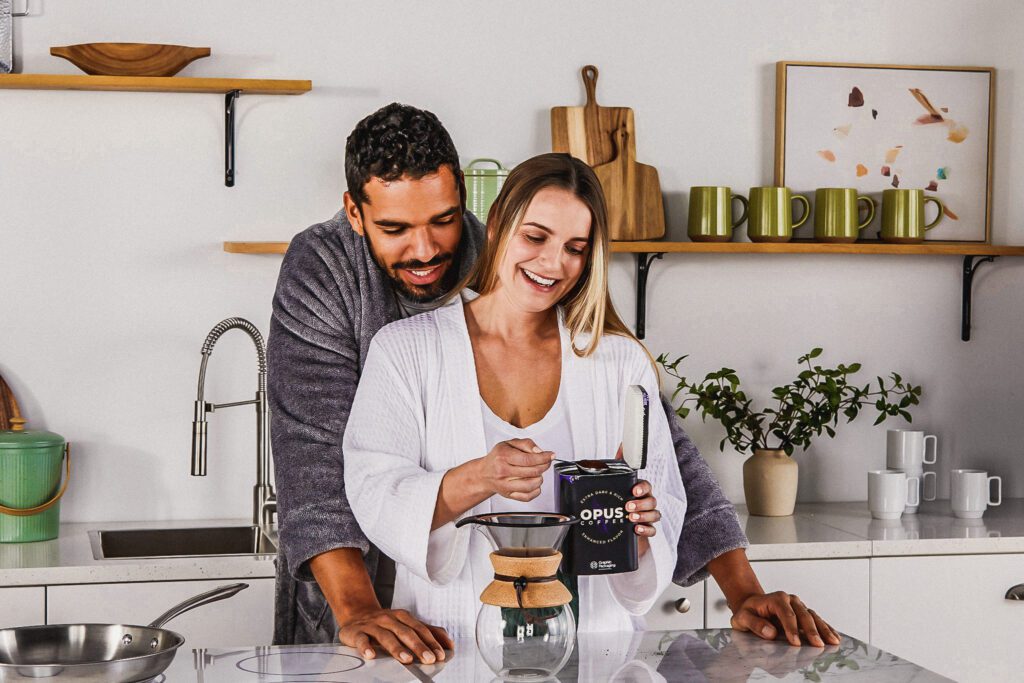
Sustainable Fiber-Based Retail Containers and Canisters

Plastic-Replacement Innovations in Action

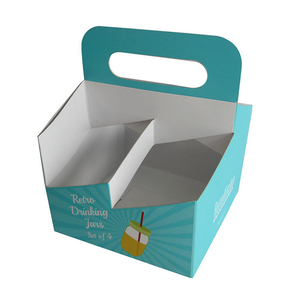
Retail giants and FMCG leaders are aggressively transitioning from plastic rings and heavy PVC shrink films toward fiber-based clip-style carriers (such as paperboard multipacks) and barrier-lined paperboard trays. By combining high-definition 3D lens graphics, tactile embossing, and laser-perforated easy-open tabs, custom fiber packaging elevates shelf presence while lowering carbon taxes across European markets.

Strategic Sourcing Insights

Future Procurement Trends: Retail Packaging (2025–2030)

How B2B procurement leaders and supply chain directors must adapt to shifting regulations and technological disruption.
Luxury Packaging Finishes and Structural Enhancements

1. Monomaterialization for Closed-Loop Circularity

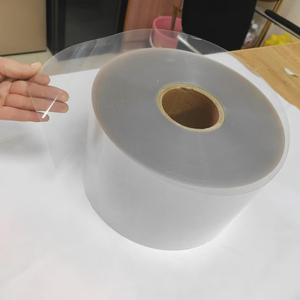
Multi-layer composite plastics are rapidly being phased out in favor of Mono-PE and Mono-PET flexible rollstock films. Procurement departments are prioritizing packaging suppliers capable of delivering high-barrier properties in single-polymer structures that fit existing municipal recycling streams without sacrificing shelf life.

2. Smart Packaging & Anti-Counterfeiting Integration

With cross-border e-commerce expanding exponentially, retail packaging is adopting embedded QR codes, invisible digital watermarking, and tamper-evident fiber structures. This satisfies both consumer desire for product provenance and enterprise demands for supply chain serialisation.

3. Automated High-Speed Line Compatibility

As labor costs rise globally, packaging materials must perform flawlessly at extreme line speeds. Custom corrugated airplane boxes, multipack beer carriers, and thermoforming webs must maintain precise gauge consistency to eliminate machine downtime and seal failures.

Procurement Knowledge Base

Frequently Asked Questions (FAQ) for B2B Buyers

Everything global procurement teams need to know regarding compliance, customization, MOQs, and technical support.

Why is CE Certification essential for custom retail packaging suppliers?
CE Certification verifies that custom retail packaging complies with European Union health, safety, and environmental protection directives (such as Directive 94/62/EC). For international exporters, CE certification guarantees that packaging materials—ranging from stretch films to corrugated shipping cartons—can enter European markets without regulatory bottlenecks or customs rejections.
What custom branding and printing options are available for corrugated boxes and paperboard carriers?
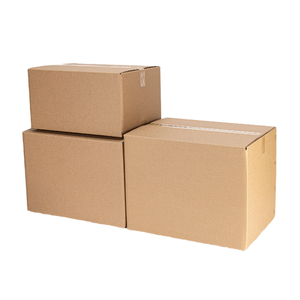
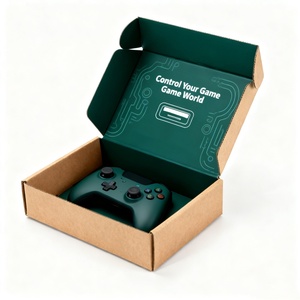
We offer comprehensive custom print enhancements including 8-color flexographic printing, high-definition offset printing, spot UV coatings, foil stamping, tactile embossing, 3D lens holographic effects, and matte/gloss lamination. Custom dimensions, die-cut windows, and structural load testing are tailored to your exact SKU parameters.
How do high-barrier PA/EVOH/PE thermoforming films extend food shelf life?
PA (Polyamide) provides exceptional mechanical strength and puncture resistance; EVOH (Ethylene Vinyl Alcohol Polymer) acts as a microscopic barrier against oxygen and gas transmission; PE (Polyethylene) ensures clean, leak-proof heat sealing. This co-extruded multi-layer construction prevents oxidation and dehydration in perishable items such as meat, cheese, and fresh food products.
What are the Minimum Order Quantities (MOQ) and lead times for custom retail packaging orders?
MOQs vary based on structural specifications. For standard low-MOQ corrugated airplane boxes and custom printed e-commerce cartons, production starts as low as 500–1,000 units. For specialized flexible rollstock films and jumbo LLDPE stretch film rolls, MOQs are determined by weight (typically 500 kg). Standard export lead time ranges between 10 to 18 business days post artwork approval.
Can your packaging materials run on existing customer packaging machinery?
Yes. Our materials are engineered for universal operational flexibility. Whether operating high-speed automated cartoning systems, horizontal form-fill-seal (HFFS) wrappers, or pallet stretch wrapping turntables, our films and board grades are calibrated for optimal coefficient of friction (COF) and thermal seal windows.
How do you support sustainability and plastic-reduction corporate mandates?
We provide full lifecycle sustainability assessments. Options include FSC-certified virgin paperboard, high-content post-consumer recycled (PCR) plastics, 100% recyclable mono-materials, commercially compostable barrier coatings, and plastic-replacement structures designed to eliminate shrink films and PVC blister packs.

Elevate Your Retail Packaging Ecosystem Today

Partner with a CE-certified, world-class packaging manufacturer. Contact our senior engineering team to audit your current packaging specs, request free samples, or receive a competitive factory-direct quotation.