
Explore our CE-compliant, structural-tested paperboard bottle carriers engineered for retail durability, automated packing lines, and brand elevation.
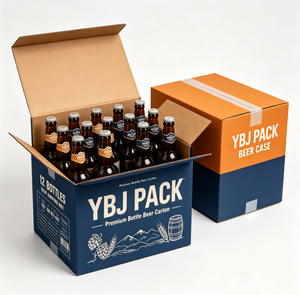
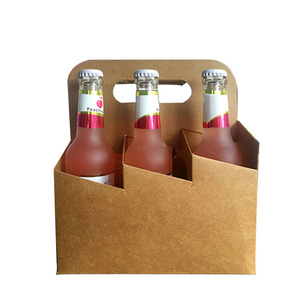
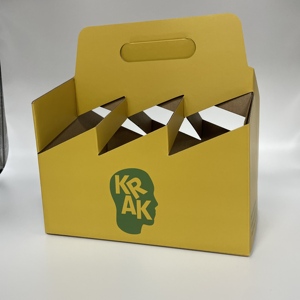
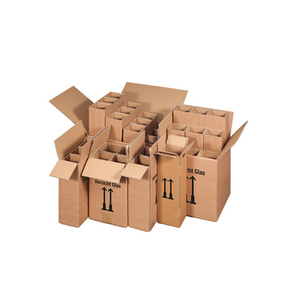
Verified performance metrics driving packaging security, operational efficiency, and circular sustainability.
In modern fast-moving consumer goods (FMCG) logistics, liquid container secondary packaging acts as both a crucial structural barrier and a primary brand touchpoint. As global beverage brands, craft breweries, winemakers, and commercial beverage bottlers shift away from single-use plastic shrink wrap and plastic ring multipacks, CE Certified Bottle Carrier Cartons have emerged as the global benchmark for safety, sustainability, and retail performance. Engineering a carrier carton that safely transports heavy glass or aluminum containers requires precise paperboard selection, specialized fiber alignment, moisture-resistant barrier coatings, and exact ergonomic die-cutting.
Technical Insight: A standard 6-pack of 330ml glass beer bottles exerts a static vertical mass load of over 2.1 kg, alongside dynamic shear forces during transit. CE Certification in bottle carrier manufacturing guarantees that the packaging meets European Union health, safety, and environmental protection standards (including Directive 94/62/EC on Packaging and Packaging Waste), ensuring high tensile strength at the handle junction, zero drop-out failure, and non-toxic chemical composition.
The foundation of an industrial-grade bottle carrier carton lies in substrate selection. Unlike standard folding cartons, multi-pack beverage carriers require high-yield tear resistance and burst strength under varying relative humidity (RH) conditions. Leading OEMs and packaging engineers utilize Coated Unbleached Kraft (CUK) or Solid Unbleached Sulfate (SUS) paperboards, recognized for their long softwood fibers that provide superior stiffness and tear resistance.
When wet-strength resins are integrated into the paperboard matrix during the pulping stage, the carton retains up to 45% of its tensile strength even when submerged in condensation ice buckets or chilled retail environments. For lighter beverage applications or gift pack boxes, micro-flute corrugated structures (E-Flute and F-Flute) offer exceptional cushioning, preventing bottle-to-bottle clinking and reducing glass breakage rates by over 98% during parcel shipping.
Handle failure is the primary point of structural breakdown in consumer multipacks. To achieve CE compliance and ensure user safety, our engineering team utilizes finite element analysis (FEA) to model load distributions across double-wall gable handles, reinforced die-cut center straps, and auto-bottom structures.
By incorporating multi-ply paperboard fold-overs at the handle apex, stress is evenly transferred across the vertical side walls rather than concentrated at the die-cut corner notches. Furthermore, bottom-locking mechanisms—such as crash lock bottoms, 4-corner glued bottoms, and interlocking tab closures—are designed to support dynamic load factors exceeding 300% of nominal beverage weight under rapid vertical displacement tests.
The following engineering matrix outlines the technical parameters available for custom industrial bottle carrier production:
| Carrier Type | Recommended Substrate | Board Caliper / Flute | Bursting Strength (Mullen) | Primary Feature & Coating |
|---|---|---|---|---|
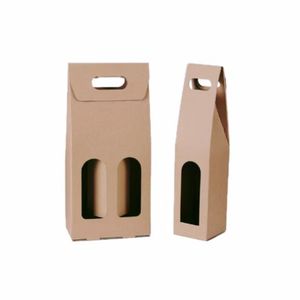
| 2 / 4 Pack Wine Gift Carrier | Solid Bleached Sulfate (SBS) / CUK | 18pt - 24pt (450gsm - 600gsm) | 250 - 320 PSI | Soft-touch matte, foil stamping, partition dividers |
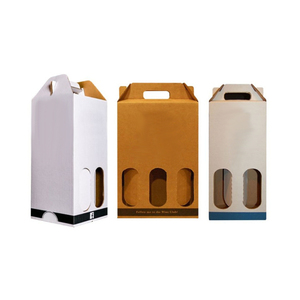
| 6 Pack Basket Bottle Carrier | Coated Unbleached Kraft (CUK) | 20pt - 28pt (500gsm - 700gsm) | 350 - 450 PSI | High wet-strength resin, double-reinforced handle |
| 12 Pack Beer / Can Master Shipper | E-Flute / B-Flute Corrugated | 1.5mm - 3.0mm thickness | 400 - 550 PSI | High ECT (Edge Crush Test), drop-resistant corners |
| Waterproof Juice / Dairy Gable Box | PE Coating / Aqueous Barrier Board | 22pt - 26pt (550gsm - 650gsm) | 300 - 400 PSI | Food-grade PE/Biopolymer lining, leak-proof bottom |
As global supply chains adapt to tighter environmental regulations and changing retail requirements, secondary packaging procurement is undergoing three major structural shifts:
A. Transition to Plastic-Free Fiber Solutions: Legislative mandates such as the EU Packaging and Packaging Waste Regulation (PPWR) are forcing brands to eliminate single-use plastic multipack rings and shrink films. Fiber-based alternatives—including clip-style top holders (such as KeelClip solutions) and fully enclosed paperboard cartons—are quickly becoming industry standards for beverage brands worldwide.
B. Machine Integration & High-Speed Automation: Modern bottling and canning plants operate filling lines at speeds ranging from 600 to 1,500 units per minute. Packaging buyers require carrier cartons designed to perform flawlessly on high-speed automated machinery (including basket formers, sleeve wrappers, and end-load cartoners). Precision die-cutting, controlled scoring depths, and consistent carton flat-blank geometry prevent jamming, de-risking high-speed packing operations.
C. Functional Bio-Coatings & Water-Based Barrier Systems: Traditional polyethylene (PE) laminations are increasingly being replaced by bio-based and aqueous barrier coatings. These next-generation coatings provide excellent grease and moisture resistance while allowing the carrier carton to be fully repulped and recycled within standard paper recycling systems (FSC and PEFC certified).
Combining vertically integrated paperboard manufacturing with advanced machinery systems and award-winning design.
As an industry leader in consumer packaging solutions, our integrated manufacturing framework provides a continuous supply chain from raw fiber pulping to converted, high-performance packaging. Our recognition across global industry rankings validates our corporate transparency, operational ethics, and sustainable innovations:
By uniting paperboard production, structural packaging design, high-definition flexographic/offset printing, and integrated machinery engineering under a single partnership, we help global buyers consolidate supply chains, cut total cost of ownership (TCO), and ensure consistent packaging quality across global markets.
Clear, technical answers to common questions about custom bottle carrier cartons, CE certification, production lead times, and machinery compatibility.
Connect directly with our packaging engineers and enterprise procurement specialists to request custom die-lines, structural samples, or machine integration audits.
Contact Us